Export-Grade Corporate & Uniform Apparel Catalog
Explore our factory-direct wholesale uniform collections engineered for international enterprise deployments, hospitality chains, and private label apparel brands.
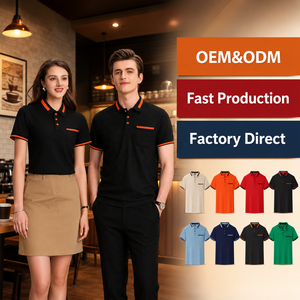
Wholesale Restaurant Hotel Front Desk Polo Shirts Custom Printed Logo Server Waitstaff Uniforms Cost-effective Factory Direct
Contact Us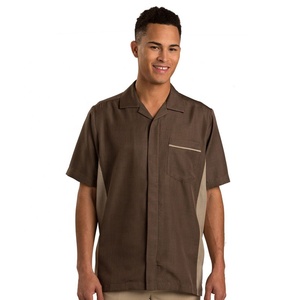
Wholesale Customized Men's Short Sleeve Hotel Staff Uniform Salon Housekeeping Service Waiter Cleaning Uniform Scrub Shirt
Contact Us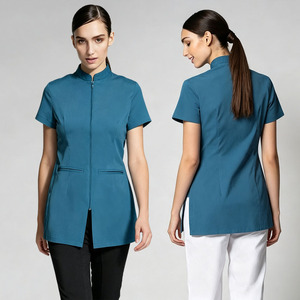
Custom Work Wear Beauty Salon Spa Uniform Hotel Uniforms Spa Female Customize Woven For Women Scrubs Luxury Uniform
Contact Us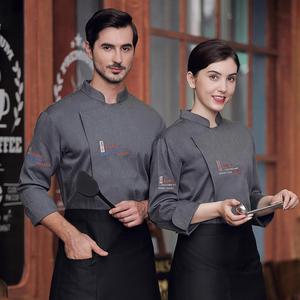
Wholesale Customized logo Restaurant Chef Uniform Long Sleeves Hospitality Chef Cloth for Kitchen and Hotel
Contact Us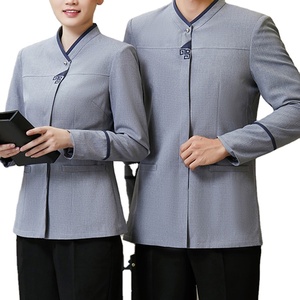
Women and Men Wholesale Hotel Work Clothes Housekeeping Restaurant Jacket Uniforms Long Sleeve Uniform Top with Customized Logo
Contact Us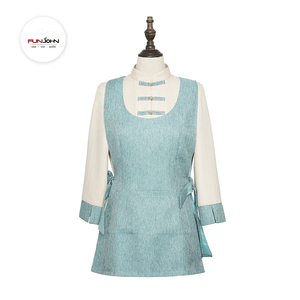
Women's 2pcs Long Sleeve 100% Polyester Housekeeping Uniform Hotel & Airport Custom Sizes OEM Service 7-Day Sample
Contact Us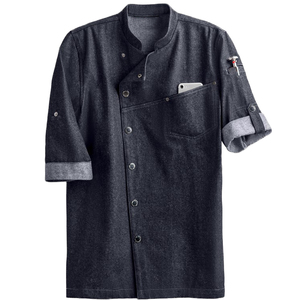
Fashion Wholesale Blue Black Custom logo Restaurant Hotel Long Sleeve Denim Chef Jacket Uniform
Contact Us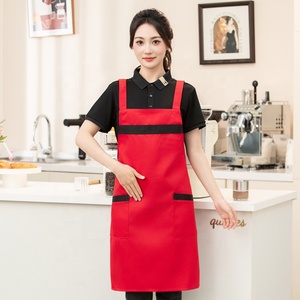
Factory Direct Sales of Professional Hotel and Restaurant Aprons, Catering Chef Uniforms, Kitchen Staff Work Clothes, Unisex
Contact UsExecutive Whitepaper: The Strategic Advantage of Sourcing Wholesale Corporate Polo Shirts from India
Understanding supply chain resilience, cotton yarn purity, advanced knit construction, and total cost of ownership (TCO) optimization for global B2B procurement managers.
In today's interconnected global market, corporate attire is no longer merely a functional requirement; it is a direct extension of a brand’s visual identity and operational culture. Organizations spanning technology conglomerates, luxury hospitality chains, financial institutions, and logistics leaders require custom uniform solutions that harmonize aesthetic elegance with rigorous industrial durability. Among various apparel categories, the corporate polo shirt stands out as the global standard for smart-casual enterprise wear.
As a leading Wholesale Corporate Polo Shirts Exporter & Exporters in India, Vihaan International provides an authoritative analysis of why global procurement directors are shifting their sourcing hubs from traditional Southeast Asian markets to India. Backed by an established textile heritage, complete vertically integrated supply chains from raw cotton ginning to finished garment export, and strict compliance with ISO 9001:2015 frameworks, Indian garment manufacturers deliver unmatched information gain and tangible value to global buyers.
Fabric Technical Specifications & Material Engineering
A comparative analysis of cotton yarn grades, GSM density, weave types, and performance finishes engineered for corporate workwear longevity.
100% Combed Cotton Pique
Spun from extra-long staple Indian cotton (Shankar-6 & MCU-5). Superior breathability, ultra-soft hand feel, and natural hypoallergenic properties ideal for warm climates and office environments.
- Yarn Count: 24s / 30s double-ply
- Weight Range: 200 – 240 GSM
- Bio-washed for zero surface fuzz
CVC & PC Poly-Cotton Blends
Engineered ratio blends (60% Cotton / 40% Polyester or 65/35) delivering maximum dimensional stability, crease resistance, and structural longevity through hundreds of industrial wash cycles.
- Shrinkage Control: < 3% (ISO 6330)
- Pilling Resistance: Grade 4+ (ASTM D3512)
- Weight Range: 180 – 260 GSM
Performance Dri-FIT & Spandex
Micro-polyester honeycomb mesh infused with 5% Elastane/Spandex. Features capillary moisture-wicking and SILVADUR™ silver-ion antimicrobial treatments for active personnel.
- Moisture Management: Quick-Dry < 15 mins
- UPF Protection: UPF 50+ Sun Shield
- Weight Range: 160 – 200 GSM
| Fabric Material Grade | Common Weaver Structure | Target Application | Color Fastness Rating | Tensile Strength (N) |
|---|---|---|---|---|
| 100% Super Combed Cotton | Classic Honeycomb / Pique Knit | Executive Corporate & Boardroom Wear | Grade 4.5 (ISO 105-B02) | ≥ 350 N |
| CVC 60/40 Premium Blend | Double Pique / Ottoman Knit | Front Desk & Customer Relations | Grade 4-5 (ISO 105-C06) | ≥ 480 N |
| Poly-Cotton 65/35 Heavy Duty | Flat Knit / Interlock Structure | Industrial Field Operations & Logistics | Grade 4.5 (Industrial Wash) | ≥ 550 N |
| Micro-Poly Spandex Active | Jacquard Mesh / Birdseye Knit | Aviation Ground Staff & Outdoor Hospitality | Grade 4.0 (Perspiration Fastness) | ≥ 420 N |
Advanced Logo Branding & Customization Technologies
Translating complex enterprise brand guideline assets onto textiles with high-definition precision, color pantone fidelity, and wash-tested durability.
1. High-Density Tajima Embroidery
Utilizing multi-head automated Japanese Tajima embroidery machinery capable of rendering up to 15,000 stitches per logo. We deploy Madeira German poly-neon threads that resist chlorine bleaching, sunlight fading, and high-temperature laundering.
2. 3D Rubberized Silicone Transfer
Ideal for contemporary tech firms and sleek sports-corporate branding. Raised 3D silicone transfers offer crisp matte or gloss dimensional effects, bonded thermally to withstand flex stress without cracking or peeling over long-term use.
3. Eco-Friendly Plastisol & Water-Based Screen Print
For large chest prints, back logos, or promotional event bulk orders. Our GOTS-certified water-based inks offer a zero-hand-feel finish, while phthalate-free plastisol delivers razor-sharp vector line reproduction matched to exact Pantone (PMS) colors.
4. Custom Garment Trims & Hardware
Complete private label customization: engraved laser buttons (laser-etched corporate logos), contrast placket piping, custom dyed-to-match rib collars, woven neck labels, soft-touch satin care tags, and branded polybag packaging.
Hyper-Localized Industry Application Scenarios
Custom uniform engineering matched to specific operational stress, ergonomic demands, and environmental climates worldwide.
Corporate IT & Financial Hubs
In technology parks across Gurgaon, Bengaluru, London, and Silicon Valley, enterprise polos require a modern tailor-fit silhouette. We combine 220 GSM bio-washed cotton with lycra-reinforced collars that prevent collar curl (the infamous "bacon collar" effect) even after multiple dry cleaning cycles.
5-Star Luxury Hospitality & Spas
Front desk managers, concierges, and wellness spa staff in Dubai, Maldives, and Paris demand breathable luxury. Our specialized woven and knitted hospitality polo shirts incorporate silk-touch finishes, stain-release treatments (Teflon™ coating), and hidden placket designs for understated elegance.
Field Operations & Retail Chains
For retail floor staff, logistics crews, and service technicians, garments face daily abrasion. Our high-tensile CVC double pique polos feature reinforced twin-needle stitching at stress points (armholes and side vents), ensuring high tear strength and zero color bleeding under harsh lighting.
Localized Market Trends Shaping Uniform Sourcing
Key macro shifts in sustainability, digital supply chain tracking, and smart fabric integration impacting global bulk procurement strategies.
Trend 01
Recycled PET & Organic Circularity
Global corporate ESG mandates require procurement officers to audit carbon footprints. Sourcing polo shirts made from GOTS-certified organic cotton blended with rPET (recycled plastic bottles) allows enterprises to fulfill sustainability benchmarks without sacrificing garment hand-feel.
Trend 02
Low MOQ Private Label Flexibility
Traditional garment factories enforced 5,000-unit minimums per colorway. Modern agile exporters in Gurgaon provide scaled tiered production starting from 200-500 units, enabling fast-growing enterprise startups and boutique chains to order custom customized apparel without over-capitalizing on inventory.
Trend 03
Digital Twin Sampling & 3D Prototyping
Before fabric cutting begins, 3D digital garment renders allow international buyers to approve seam placements, logo scaling, and color contrasts virtually. This accelerates pre-production sample approvals from weeks down to 48 hours.
Trend 04
Antimicrobial & Odor-Shield Finishes
Post-pandemic workplace standards prioritize employee health. Modern corporate polos incorporate bio-based antimicrobial coatings that inhibit odor-causing bacteria, keeping staff fresh through 12-hour active shifts.
Vihaan International: Manufacturing Infrastructure & Export Quality Protocol
Operating from a state-of-the-art facility in Gurgaon, Delhi NCR, Vihaan International integrates cutting-edge Japanese machinery with rigorous quality management systems.
Our 5-Stage In-Line Quality Inspection Standard
To guarantee zero-defect shipments across international borders, every order undergoes our mandatory 5-point quality audit compliant with AQL 2.5 parameters:
Fabric & Raw Material Audit
GSM verification, 4-point fabric inspection system for weaving defects, color batch lab-dip matching under D65 light source.
CAD Pattern Precision Cutting
Automated pattern marker creation to maximize fabric yield and ensure dimensional consistency across size sets (XS to 5XL).
In-Line Stitching & Assembly
JUKI industrial lockstitch machines monitoring seam strength, SPI (stitches per inch) count, and tension alignment every 3rd operation.
Branding & Wash Testing
Embroidery pull-tests, logo alignment check, and random sample wash-and-dry cycles to verify color fastness and zero shrinkage.
Frequently Asked Questions (FAQ) for Global B2B Apparel Sourcing
Clear, authoritative answers addressing procurement terms, export logistics, custom sampling, and quality parameters.
What is the typical Minimum Order Quantity (MOQ) for custom corporate polo shirts?
Our standard MOQ for wholesale custom corporate polo shirts starts at 200 to 500 pieces per design/colorway depending on fabric customization. For stock fabric colors with custom embroidery or logo printing, we offer lower starter tiers for growing enterprises and specialized hospitality projects.
What are the bulk production lead times for international export orders?
Pre-production counter samples are developed and dispatched within 5 to 7 business days via international express courier. Upon sample sign-off and lab-dip approval, bulk manufacturing turnaround ranges between 15 to 25 calendar days depending on order volume and branding complexity.
Which export shipping terms and trade documentation do you support?
Vihaan International is fully IEC (Import Export Code) registered and DGFT compliant in India. We regularly fulfill orders under FOB (Free on Board - Nhava Sheva / ICD Tughlakabad), CIF (Cost, Insurance & Freight), and DDP (Delivered Duty Paid) terms to buyers across the USA, UK, EU, Canada, Australia, and the Middle East, handling all customs documentation and Certificate of Origin processing.
How do you ensure color consistency across multiple re-orders over time?
We utilize standardized Pantone Matching System (PMS) color codes and store digital lab-dip spectral data for every client order. All yarn dyeing is executed in ISO-certified dye houses using reactive dyes, guaranteeing batch-to-batch color matching accuracy (Delta E < 0.8) for seamless multi-year uniform program rollouts.
Can we request custom fabric weights (GSM) and proprietary material blends?
Yes. As a custom uniform manufacturer, we offer mill-customized fabric knitting. We can engineer specific fabric weights from 160 GSM lightweight knits to 260 GSM heavy-duty pique, as well as custom blends including Organic Cotton, Bamboo-Cotton, Recycled Polyester, and Spandex elastane combinations.
Do you supply full uniform packages for hotels and multi-department enterprises?
Absolutely. Beyond polo shirts, our Gurgaon facility manufactures turnkey uniform collections including front desk formal blazers, housekeeping scrubs, chef coats, aprons, spa tunics, and tactical workwear jackets, enabling clients to consolidate vendor sourcing under one reliable export manufacturer.
Ready to Upgrade Your Corporate Uniform & Apparel Sourcing?
Partner with India’s trusted wholesale garment exporter. Request custom fabric swatch books, instant bulk price quotations, or virtual factory tours today.