Corporate Polo T-Shirt Manufacturing: The Definitive Global Procurement & Engineering Blueprint
A comprehensive B2B sourcing guide written for procurement directors, brand founders, and global apparel buyers. Discover fabric GSM selection, anti-pilling yarn blends, precision embroidery engineering, and export-grade supply chain protocols from India’s ISO 9001:2015 certified manufacturer.
1. Executive Procurement Overview: Why Corporate Polo T-Shirt Manufacturing Demands Engineering Precision
In modern enterprise management, the corporate polo t-shirt has evolved far beyond basic promotional merchandise. It serves as the primary visual touchpoint of corporate identity, a physical extension of employer branding, and a crucial component of workplace ergonomic comfort. Whether deployed across global IT service hubs, luxury hospitality front-of-house teams, high-tech logistics operations, or regional field sales forces, a corporate polo must withstand rigorous commercial laundering, resist color fading, maintain structural collar integrity, and present a crisp, authoritative silhouette.
However, global procurement officers and apparel brand sourcing executives frequently encounter systemic bottlenecks when navigating Corporate Polo T-Shirt Manufacturing. Common industry pain points include collar curling (the dreaded "bacon collar"), fabric pilling after fewer than 10 wash cycles, seam twisting due to improper fabric relaxation before cutting, and erratic color variance across bulk dye lots.
Headquartered in Gurgaon, Delhi NCR—the heart of India's textile innovation and export infrastructure—Vihaan International operates as a tier-1 custom corporate uniform manufacturer in India. Backed by ISO 9001:2015 accreditation, an internal capacity exceeding 20,000 units per month, and an export footprint spanning over 15 countries (including the USA, UK, Canada, France, Germany, and the UAE), Vihaan International bridges the gap between raw textile science and enterprise-grade garment execution.
Information Gain Insights for B2B Sourcing Managers
Unlike conventional garment traders who rely on off-the-shelf ready stock, genuine OEM/ODM corporate polo t-shirt manufacturing requires controlling three non-negotiable variables: Yarn Twist Factor (tpi) to eliminate torque and body bias, Comb Ratio & Fiber Staple Length to minimize surface fuzz, and Heat-Setting Thermofixation during dyeing to restrict shrinkage to under 3% under standard ISO 6330 testing.
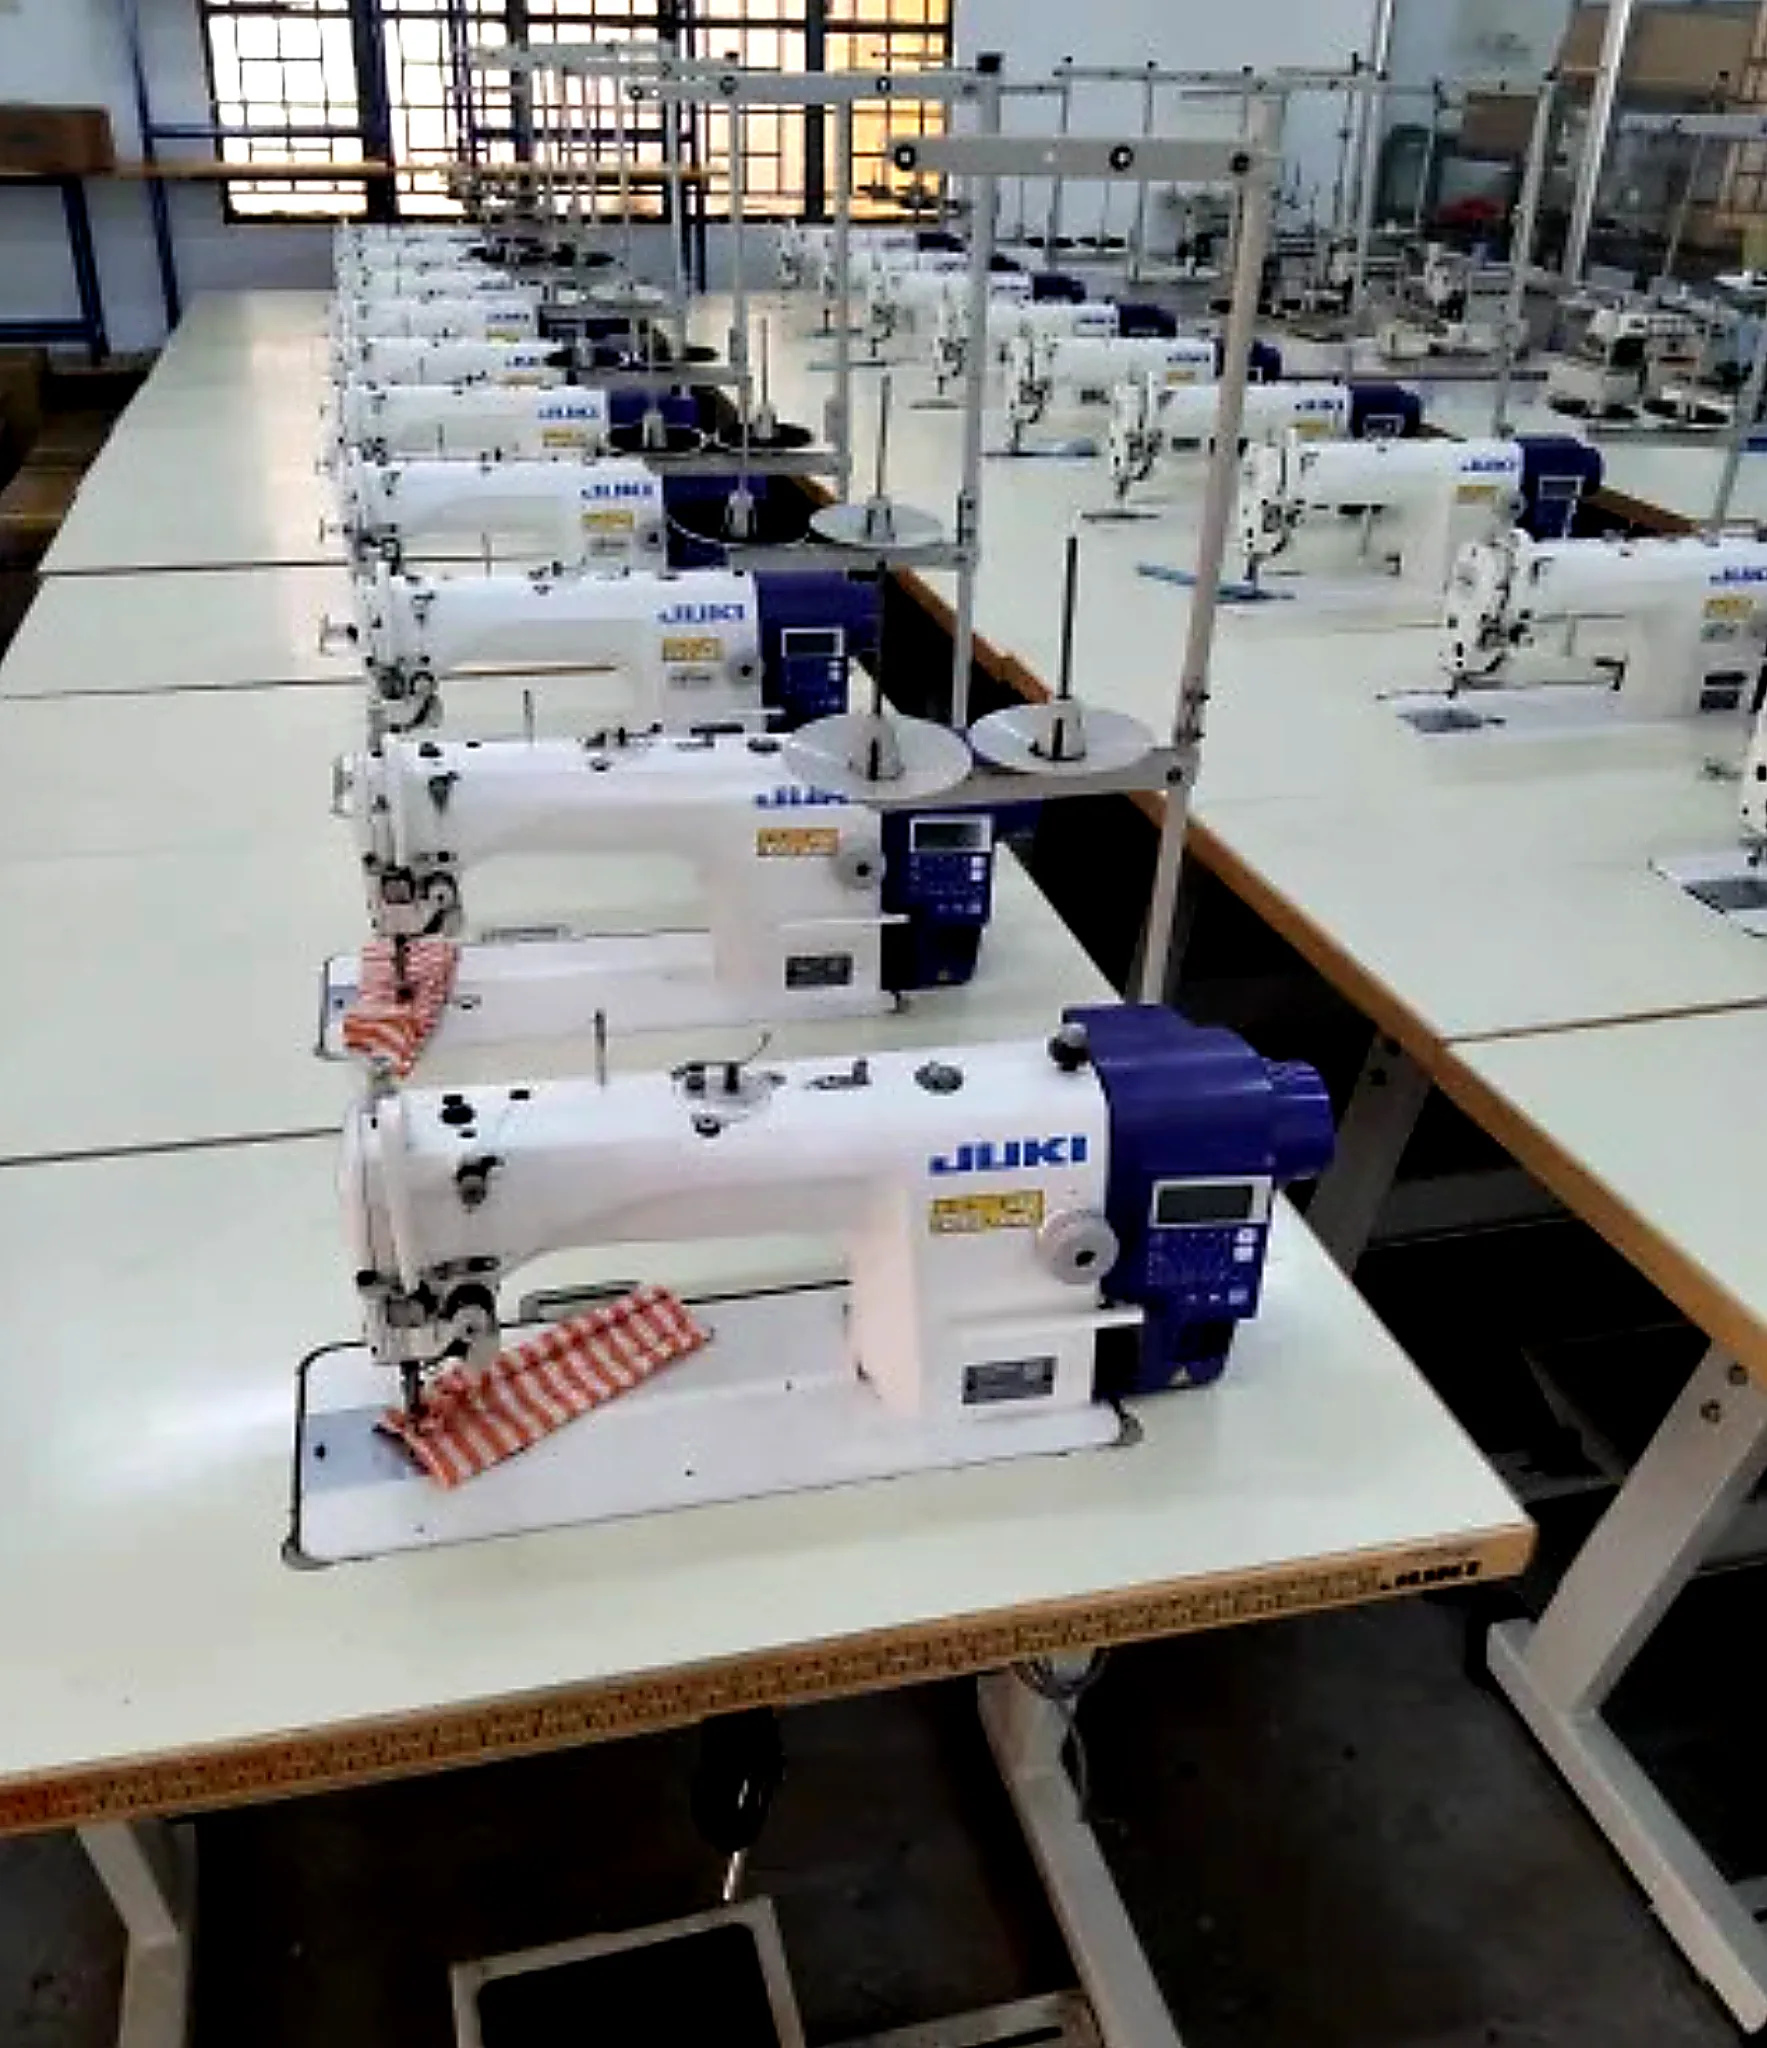
2. Product Recommendations & Specification Matrix for Enterprise Buyers
To align with diverse operational environments and organizational tier structures, Vihaan International manufactures five distinct categories of corporate polo t-shirts. Each product tier is engineered using specific yarn counts, knitting gauge structures, and finishing treatments.
1. Executive Cotton-Pique Polo
Designed for executive leadership, client-facing consultants, and premium retail staff requiring an elevated aesthetic.
- Composition: 100% Super-Combed Supima / Egyptian Cotton
- Fabric Weight: 220 – 240 GSM Honeycomb Pique
- Collar Spec: Jacquard Collar with Anti-Roll Stiffening Insert
- Finish: Bio-Wash + Silicon Softener Treatment
- Branding: High-Density 3D Micro-Embroidery
2. Tech-Performance CoolMesh Polo
Tailored for tech enterprise campuses, field service engineers, and active corporate promotional events.
- Composition: 60% Combed Cotton / 40% Polyester Mesh
- Fabric Weight: 180 – 200 GSM Interlock / Birdseye
- Collar Spec: Self-Fabric Collar with Fuse Interlining
- Finish: Wicking finish + Anti-Bacterial Silver-Ion
- Branding: Reflective Heat-Transfer / Breathable Screen Print
3. Heavy-Duty Industrial Uniform Polo
Built for logistics, warehousing, aviation ground crew, and industrial plant operations.
- Composition: 65% Polyester / 35% Cotton (Poly-Cotton CVC)
- Fabric Weight: 230 – 250 GSM Heavy Double-Pique
- Collar Spec: 1x1 Heavy Ribbed Knit with Double-Needle Seams
- Finish: Stain Release + Color-Lock Fastness Grade 4.5
- Branding: Industrial Washable Direct Embroidery
Technical Comparison: Selecting the Right Fabric Architecture
The table below provides a comparative analysis of the primary fabric formulations utilized in custom corporate polo manufacturing at Vihaan International:
| Fabric Blend | GSM Range | Breathability | Shrinkage Rate | Color Fastness | Ideal Application |
|---|---|---|---|---|---|
| 100% Combed Cotton Pique | 200 - 240 | Excellent (5/5) | < 3.0% (Pre-Shrunk) | Grade 4.0 | Executive Corporate Wear, Luxury Retail |
| 60/40 CVC (Chief Value Cotton) | 190 - 220 | Very Good (4/5) | < 1.5% | Grade 4.5 | Standard Corporate Uniforms, Tech Hubs |
| 65/35 PC (Poly-Cotton Blend) | 210 - 250 | Moderate (3/5) | < 1.0% | Grade 4.8 (High Durability) | Logistics, Operations, High-Wash Duty |
| Cotton-Modal Elastane Blend | 180 - 210 | Superior (5/5) | < 2.5% | Grade 4.2 | Premium Boutique Brands, Private Label |
3. Future Procurement Trends in Corporate Polo T-Shirt Manufacturing (2026–2030)
The global corporate workwear landscape is undergoing a structural paradigm shift. Driven by international ESG (Environmental, Social, and Governance) compliance directives, hybrid work models, and rapid advancements in textile chemistry, global buyers are redefining their sourcing criteria. Procurement directors must anticipate the following key trends:
A. Decarbonized & Circular Textile Sourcing
Multinational corporations headquartered in the US and Europe are mandated to report Scope 3 supply chain carbon emissions. Consequently, demand is accelerating for corporate polo t-shirts manufactured from GRS-Certified (Global Recycled Standard) Recycled Polyester blended with GOTS-Certified Organic Cotton. Zero-liquid-discharge (ZLD) dyeing processes, which recycle 95%+ of process water, are becoming a prerequisite for tier-1 supplier qualification.
B. Smart Fabric Finishes & Wearable Comfort Science
The modern corporate workforce demands functional versatility. Future-ready corporate polos integrate permanent non-chemical moisture management (hydrophilic inner surface, hydrophobic outer surface), UPF 50+ ultraviolet protection for outdoor field staff, and thermo-regulating phase-change materials (PCM) that adapt to air-conditioned offices and warm outdoor environments seamlessly.
C. Micro-Customization and On-Demand Replenishment Hubs
Large enterprises are abandoning rigid 12-month advance bulk purchasing models in favor of agile, quarter-by-quarter replenishment cycles. By partnering with vertically integrated manufacturers in India who offer digital CAD pattern grading and flexible minimum order quantities (MOQs from 500 units for corporate programs), enterprises can order customized colorways per department without locking up working capital in excess inventory.
4. Engineering Excellence: Fabric Science & Construction Innovations
What distinguishes an ordinary polo shirt from a high-performance corporate uniform garment? The secret lies in the underlying structural construction and mechanical finishing techniques executed during manufacturing.
1. Collar Engineering and Shape Retention
The collar is the most vulnerable component of a polo shirt. Cheaply manufactured polos utilize single-ply flat knits that curl after a few washes. Vihaan International utilizes dual-ply jacquard collar knitting integrated with low-melt thermoplastic fusible interlinings or high-density elastane rib inserts. This guarantees that the collar maintains its flat, crisp arch even after 50 industrial wash cycles.
2. Anti-Torque Knitting & Pattern Balance
Fabric torque occurs when the side seams of a polo shirt twist toward the front or back after laundering, caused by unbalanced yarn twist during circular knitting. To prevent torque, our manufacturing protocol enforces S-twist and Z-twist yarn ply balancing combined with a mandatory 24-hour fabric tension relaxation period prior to automated CAD spreading and cutting.
3. High-Density Embroidery & Branding Integrity
A corporate logo represents a brand's integrity. We utilize multi-head Tajima and Barudan computerized embroidery machinery operating at up to 1,000 stitches per minute. Backing stabilizers (cutaway vs. tearaway) are mathematically selected based on fabric GSM to eliminate puckering, ensuring that complex corporate emblems remain completely flat and pristine.
5. Enterprise Advantages: Why Vihaan International is India’s Premier Polo Manufacturer
Selecting Vihaan International as your manufacturing partner provides immediate access to world-class manufacturing capabilities, regulatory compliance, and end-to-end supply chain transparency:
- Gurgaon Manufacturing Hub: Located in Udyog Vihar, Phase 4, Gurgaon (Delhi NCR), our state-of-the-art facility is situated just 15 minutes from Indira Gandhi International Airport (DEL) and within close proximity to major ICD dry ports, facilitating rapid sea and air freight logistics.
- ISO 9001:2015 Quality Management System: Every production batch undergoes a rigorous 5-stage quality assurance protocol—from raw yarn testing and grey fabric inspection to in-line seam checking, iron-finishing audit, and final AQL 2.5 carton sampling.
- IEC & DGFT Export Compliance: Fully registered with the Directorate General of Foreign Trade (DGFT) and holding an active Import Export Code (IEC), we seamlessly execute export contracts under FOB, CIF, CFR, or DDP (Delivered Duty Paid) terms directly to buyer warehouses in North America, Europe, and the Middle East.
- Ethical & Audit-Ready Workplace: We strictly adhere to fair wage structures, workplace safety protocols, and zero child-labor policies. Our factory floor is open for third-party audits (SGS, Intertek, Bureau Veritas) mandated by global buyers.
Ready to Scale Your Corporate Polo Production?
Connect with our technical textile team to request fabric swatch cards, custom sample development, or a competitive bulk quotation tailored to your exact specifications.
6. B2B Procurement FAQ: Corporate Polo T-Shirt Manufacturing
Below are technical and operational answers to the most frequently searched questions asked by global apparel buyers, procurement heads, and private label apparel founders:
7. Strategic Sourcing Summary
Partnering with the right corporate polo t-shirt manufacturer is a strategic investment in your organization's brand equity and operational success. By combining advanced fabric engineering, rigorous ISO 9001:2015 quality controls, ethical production standards, and seamless international shipping logistics, Vihaan International delivers uncompromised apparel excellence from Gurgaon, India to the world.