Commercial Uniforms & Custom Apparel Range
Engineered for Australian commercial standards, hospitality durability, and corporate brand representation.
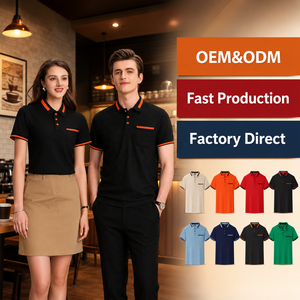
Wholesale Restaurant & Front Desk Custom Logo Polo Shirts
Contact Us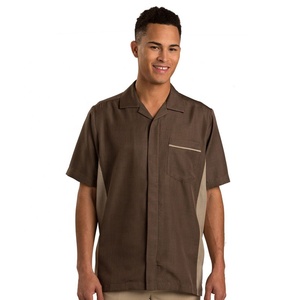
Custom Men Short Sleeve Housekeeping & Service Staff Shirts
Contact Us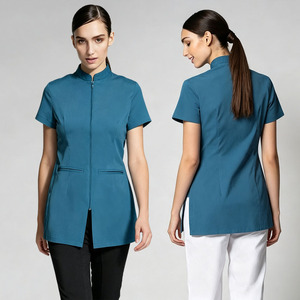
Luxury Woven Beauty Salon & Spa Ergonomic Female Uniforms
Contact Us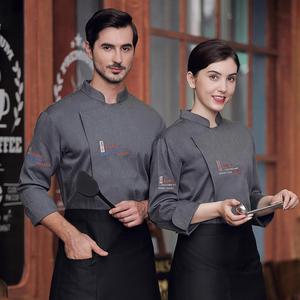
Wholesale Customized Logo Hospitality Kitchen Chef Coats
Contact Us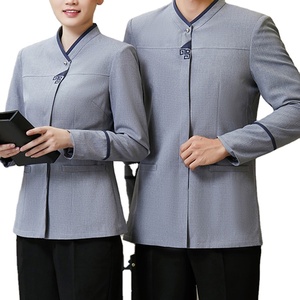
Unisex Hotel & Restaurant Housekeeping Long Sleeve Jackets
Contact Us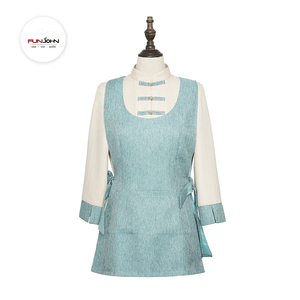
Women's 2-Piece Polyester Housekeeping & Airport Staff Uniform
Contact Us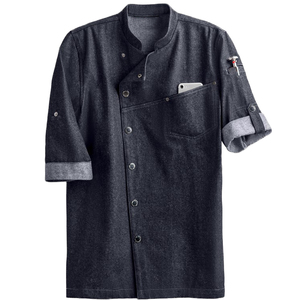
Fashion Wholesale Denim Long Sleeve Chef Uniform Jacket
Contact Us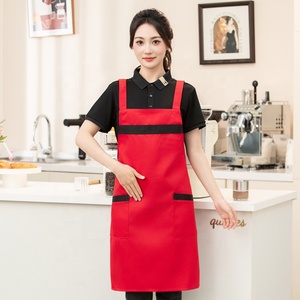
Factory Direct Professional Heavy-Duty Catering & Kitchen Aprons
Contact UsAustralian Commercial Apparel Landscape & Technical Demands
In the rapidly evolving Australian B2B landscape, corporate identity, workplace safety, and environmental stewardship have merged into a unified procurement mandate. Australian enterprise buyers—ranging from multi-site mining outfits in Western Australia to boutique hospitality groups along the Gold Coast and corporate tech hubs in Sydney’s Barangaroo—are moving away from generic off-the-shelf garments. Instead, they demand highly customized Original Equipment Manufacturer (OEM) and Original Design Manufacturer (ODM) partners capable of integrating high-performance fabric technologies with strict brand compliance.
Procurement intent analysis reveals that Australian organizations prioritize three non-negotiable pillars when contracting overseas apparel factories: Textile Durability & Comfort under harsh climate conditions, Ethical Sourcing Transparency compliant with Australia’s Modern Slavery Act 2018, and Reliable Supply Chain Logistics that mitigate sea-freight bottleneck risks to major Australian ports (Sydney, Melbourne, Brisbane, and Fremantle).
Information Gain Keyword Focus: Technical Climate Adaptation
Australia’s climate profile presents unique challenges for promotional and workwear apparel. High UV indexes necessitate AS/NZS 4399:2020 certified sun protection (UPF 50+ rating), while high humidity in Northern Queensland requires advanced moisture-wicking cool-mesh polyester blends. Our factory specializes in customized yarn-dyed fabrics and reactive screen printing engineered specifically to withstand UV degradation and frequent industrial laundering without fading or fabric pillage.
AS/NZS Compliance
Rigorous testing for UV radiation resistance (UPF 30+ to 50+), colorfastness to light, and seam burst strength according to Australian and New Zealand safety standards.
Rapid Sample Dispatch
7-day physical prototype development with air express delivery via DHL/FedEx straight to Sydney, Melbourne, or Perth headquarters for immediate fit-and-wear evaluation.
Low MOQ & Bulk Scaling
Flexible minimum order quantities starting from 200–500 units per style with seamless scaling capabilities up to 20,000+ units per monthly order cycle.
OEM vs ODM Customization & Print Technology Comparison
Evaluating printing methodologies, textile compositions, and application scenarios for Australian commercial purchasers.
| Branding Technique | Optimal Fabric Substrate | Color Durability & Wash Rating | Best Australian Application | Production Lead Time |
|---|---|---|---|---|
| Reactive Screen Printing | 100% Combed Cotton (180–220 GSM) | 50+ Commercial Washes (4.5/5 Rating) | Promotional T-Shirts, Corporate Event Merch | 10–14 Days |
| High-Density 3D Embroidery | Poly-Cotton Pique / Heavy Twill | Lifetime Garment Durability | Executive Golf Polos, Hospitality Blazers | 12–16 Days |
| Sublimation Transfer | 100% Micro-Mesh Polyester (Dry-Fit) | Zero Fading / Permanent Infusion | Sporting Clubs, Activewear, High-Vis Apparel | 7–10 Days |
| Direct-to-Garment (DTG) | Ring-Spun Organic Cotton | 30+ Standard Washes | Intricate Multi-Color Artisanal Designs | 5–7 Days |
Localized Application Scenarios Across Australian Sectors
1. Luxury Hospitality & Fine Dining (Sydney & Melbourne)
Australia’s world-class dining and premium hotel sector demands high-aesthetic, heat-resistant uniforms. Our factory manufactures double-breasted denim chef jackets with breathable underarm mesh, moisture-repellent server aprons, and refined housekeeping scrubs designed for 12-hour movement flexibility without creasing.
2. Corporate Tech & Financial Enterprises
From Sydney CBD corporate offices to tech summits in Brisbane, brand consistency across employee touchpoints is essential. We produce custom-dyed polo shirts with Pantone-matched embroidered logos, contrasting collar trims, and eco-friendly organic cotton blends that align with modern corporate sustainability goals.
3. Healthcare, Spa & Wellness Chains
Australia’s healthcare and luxury spa sector requires anti-microbial, soft-touch woven scrubs. Utilizing lightweight poly-spandex blends, our ODM team engineers ergonomic tunics with reinforced pockets and stretch panels tailored to withstand high-temperature industrial sterilization cycles.
Industrial Manufacturing Capabilities & Quality Control
As a premier OEM/ODM manufacturer, our production facility features over 50 JUKI computerized sewing stations, automated CAD pattern-cutting tables, and in-house embroidery lines. We oversee the entire garment manufacturing lifecycle—from raw yarn sourcing to final packaging—eliminating middleman markups and guaranteeing strict adherence to technical specifications.
5-Stage Quality Assurance
Every garment lot undergoes rigorous inspection: 1) Raw fabric GSM and shrinkage testing, 2) Precision CAD cutting checks, 3) In-line seam strength auditing every 3rd operation, 4) Logo placement and colorfastness verification, and 5) Final AQL 2.5 standard pre-shipment auditing.
Sustainable & Ethical Production
We operate an audit-ready, ethical facility committed to fair labor wages, non-toxic OEKO-TEX Standard 100 dyes, and GOTS-certified organic cotton. Complete supply chain traceability documentation is provided to satisfy Australian corporate governance requirements.
End-to-End Customs & Logistics
We handle all export documentation, Australian customs paperwork, tariff classification, and freight logistics under FOB, CIF, or DDP (Delivered Duty Paid) terms directly to your facility anywhere in Australia.
Frequently Asked Questions by Australian Buyers
Q: What is the typical lead time for custom promotional apparel orders shipped to Australia?
Sample production takes 5–7 working days following tech pack approval. Bulk production ranges from 15–20 days depending on order quantity. Air express shipping to Sydney or Melbourne takes 3–5 days, while ocean freight takes approximately 14–18 days.
Q: Do your garments comply with Australian Sun Protection Standards (AS/NZS 4399)?
Yes. We offer specialized outdoor fabrics explicitly woven and treated to deliver UPF 30+ to UPF 50+ protection ratings. Technical lab test certificates from accredited independent testing agencies are available upon request.
Q: Can you assist with ODM design development if we only have a rough logo draft?
Absolutely. Our in-house ODM design engineering team can create 3D virtual garment mockups, recommend technical fabrics suited for your industry, and engineer custom size grading adapted specifically for Australian sizing standards.
Q: What are your minimum order quantities (MOQ) for corporate branding?
Our standard MOQ starts at 200 pieces per design for custom woven hospitality/scrub garments and 300 pieces for custom dyed and printed polo shirts or T-shirts. We offer multi-size allocation within each batch to accommodate diverse staff requirements.
Q: How do you ensure brand color accuracy (Pantone Matching)?
We utilize precise Pantone Matching System (PMS) lab dips for fabric dyeing and computer-controlled ink mixing for screen printing, ensuring your corporate brand colors are matched with a ΔE < 1.0 color variance margin.
Ready to Upgrade Your Australian Apparel Supply Chain?
Partner with an ISO 9001 certified OEM/ODM apparel manufacturer. Contact our B2B sales engineers today for instant pricing, fabric swatches, and custom digital mockups.