Featured Wholesale Restaurant Uniform Sets
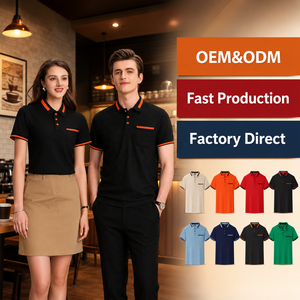
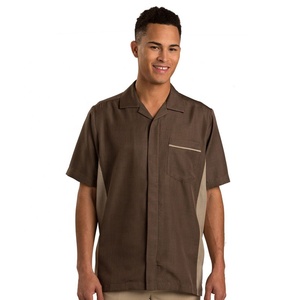
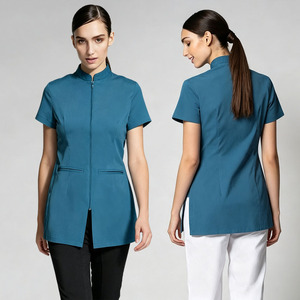
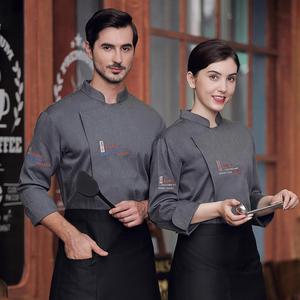
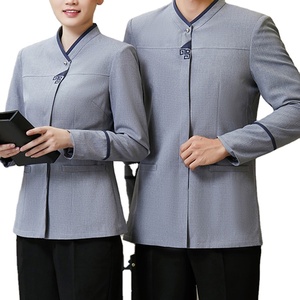
Factory-direct OEM/ODM uniform configurations engineered for hotel front desks, commercial kitchens, luxury dining, spa services, and housekeeping teams.

Global Hospitality & Restaurant Uniform Industry Trends (2025–2030)
The global commercial uniform manufacturing landscape is undergoing a structural paradigm shift driven by advanced textile engineering, stringent ISO environmental mandates, and operational cost optimization. Restaurant chains, luxury hotel groups, and international catering enterprises no longer view staff uniforms as simple consumable workwear; instead, uniforms are now evaluated as critical brand assets and functional equipment directly impacting staff performance, hygiene compliance, and corporate sustainability metrics.
1. Transition to High-Performance Smart & Technical Fabrics
Modern commercial kitchen environments present severe thermal stress, humidity, and chemical exposure (such as hot grease, detergent splatter, and organic acids). Industrial research reveals that traditional 100% cotton uniforms suffer from rapid moisture retention and fabric degradation, whereas low-grade polyester fabrics cause overheating and skin irritation. Leading B2B apparel exporters are pioneering hybrid textile blends featuring:
- Nanotech Fluid Repellency: Fluorocarbon-free C0 DWR (Durable Water Repellent) treatments that cause oil, wine, and sauces to bead up and roll off without compromising fabric breathability.
- Permanent Antimicrobial Shielding: Silver-ion and zinc-based molecular bonds woven into yarns to inhibit 99.9% of bacterial growth, eliminating persistent kitchen odors and meeting HACCP hygiene standards.
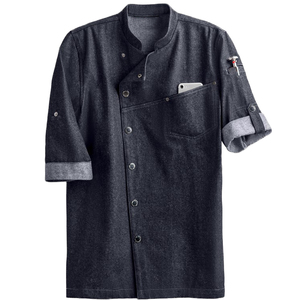
- Thermal Regulation & 3D Ventilation Mesh: Strategically positioned moisture-wicking gussets under the armpits and across the shoulder blades of chef jackets to reduce core body temperature in high-heat environments.
2. Sustainability & Circular Supply Chain Imperatives
With international buyers in North America, Europe, and the Middle East facing stringent ESG (Environmental, Social, and Governance) reporting rules, uniform exporters must align with eco-certification benchmarks. The adoption of GRS (Global Recycled Standard) certified recycled polyester (rPET) derived from post-consumer plastic bottles combined with OEKO-TEX Standard 100 non-toxic dyes has become a core procurement standard for major hotel brands like Marriott, Hilton, and Accor.
3. Ergonomic Design & Modular Unisex Uniform Configurations
Cross-departmental versatility is transforming uniform program design. Multi-unit restaurant franchises are moving away from hyper-specific department clothing toward modular uniform suites where front-desk polo shirts, waiter aprons, and housekeeping jackets share matching color palettes, trim accents, and standardized sizing scales. This modularity simplifies inventory management, lowers minimum order quantities (MOQs), and reduces safety stock carrying costs by up to 28%.
Strategic Procurement Trends & Direct-Factory Benchmarks
Procurement directors and hospitality sourcing executives are increasingly bypassing intermediate trading agencies in favor of direct-factory relationships with integrated manufacturers. Direct OEM/ODM sourcing unlocks substantial operational efficiencies, custom embroidery precision, and rigorous quality control transparency.
Comparison: Standard Commercial Uniforms vs. High-Performance Factory-Direct Uniform Sets
| Evaluation Parameter | Generic Off-The-Shelf Uniforms | Vihaan International Factory-Direct Sets |
|---|---|---|
| Fabric Engineering | Unspecified poly-cotton blends, high shrinkage rates (>5%) | Pre-shrunk (≤1.5%), custom GSM-matched technical twills and piqué knits |
| Commercial Wash Durability | 40–60 industrial laundry cycles before pilling/fading | 150+ high-temperature commercial laundry cycles (ISO 105-C06 compliant) |
| Logo & Branding Precision | Basic screen printing prone to cracking; loose thread embroidery | High-density Tajima machine embroidery & sublimated elastomeric heat-transfers |
| Customization Depth | Fixed sizes and colors; zero modification flexibility | Full OEM/ODM: custom Pantone dyed fabric, branded buttons, customized fit cuts |
| Supply Chain Integrity | Third-party reseller markup; untraceable origin | ISO 9001:2015 certified facility, IEC registered, DGFT export compliant |
Key Sourcing Drivers for Enterprise Buyers in 2025
- Pantone Color Accuracy & Batch-to-Batch Consistency: Automated spectro-photometer color matching guarantees that re-orders placed 12 months apart match brand brand colors identically.
- Rapid Prototyping & 7-Day Sampling Programs: Accelerated physical sampling allows global hospitality procurement managers to evaluate fit, seam strength, and wash resistance prior to bulk production authorization.
- Duty-Optimized & Tariff-Compliant Export Shipping: Exporters operating out of premier apparel hubs like Gurgaon, India provide full international export documentation including FOB, CIF, and DDP terms with IEC and DGFT validation.
Enterprise Manufacturing Capabilities & Quality Architecture
As an industry leader in custom corporate uniforms, hotel workwear, and women's fashion manufacturing, Vihaan International operates a state-of-the-art facility located in Udyog Vihar Phase 4, Gurgaon, Delhi NCR, India. Engineered for high-volume enterprise orders and private label fashion production, the factory integrates modern Japanese JUKI automation with traditional artisanal textile craft.
20,000+ Units Monthly Capacity
Dedicated production lines for corporate polo shirts, tailored hotel blazers, chef coats, housekeeping tunics, and heavy-duty aprons, ensuring prompt delivery during peak hospitality opening seasons.
5-Stage ISO Quality Assurance
Every production run passes through rigorous checkpoints: Raw Fabric Inspection (GSM & Colorfastness) → CAD Pattern Cutting → In-Line Stitch Density Monitoring → Logo Embroidery Verification → AQL 2.5 Final Pre-Shipment Inspection.
Global Export Compliance
Fully IEC-registered and DGFT-compliant export infrastructure serving buyers across the USA, UK, Canada, France, European Union, UAE, Saudi Arabia, and Australia with complete customs documentation.
5-Stage Precision Manufacturing Workflow
To eliminate defects and maintain strict compliance with international brand standards, our factory adheres to a continuous quality control protocol:
- Stage 1: Raw Material Audit: Fabrics undergo spectro-photometric color testing, lab dip verification, GSM weight checks, and dimensional stability wash tests.
- Stage 2: Precision CAD Patterning & Marker Making: Computer-aided design guarantees zero measurement variance across size runs (XS to 5XL) while optimizing fabric yield to support eco-friendly zero-waste targets.
- Stage 3: Automated Assembly & Reinforced Stitching: High-speed sewing machines utilizing coat core-spun threads deliver 12 to 14 stitches per inch (SPI) with double-tacked strain points on stress zones like pocket corners and armholes.
- Stage 4: Logo Application & Surface Finishing: Multi-head embroidery systems deliver crisp logo reproduction with high-lustre thread; heat presses ensure permanent vinyl and screen-printed branding.
- Stage 5: Ironing, Inspection & Barcoded Packing: 100% steam pressing, loose thread trimming, metal detector safety scanning, and individual polybag packaging labeled with SKU barcodes for direct distribution to client outlets.
Frequently Asked Questions (Procurement FAQ)
Answers to common questions from B2B buyers, procurement managers, and hospitality group sourcing executives.
Partner with India's Premier Uniform OEM/ODM Exporter
Streamline your hospitality group's procurement workflow, reduce uniform lifecycle costs, and elevate your staff's brand presentation with factory-direct custom restaurant uniform sets.
Contact Us