Featured Wholesale Corporate Polo & Uniform Series
Explore factory-direct corporate uniform solutions engineered for durability, brand consistency, and ergonomic comfort across hospitality, corporate IT, and service sectors.
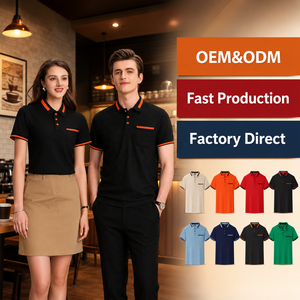
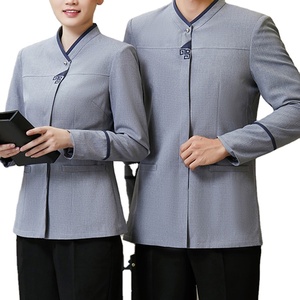
OEM/ODM Corporate Polo Shirt Manufacturing: Technical Architecture & Strategic Sourcing
In modern corporate governance and brand management, employee apparel has evolved far beyond basic workplace attire. Corporate polo shirts represent a primary physical touchpoint of enterprise identity, acting as a walking endorsement of professionalism, brand consistency, and operational rigor. For Fortune 500 enterprises, multinational tech conglomerates, luxury hotel chains, and fast-scaling retail franchises, procuring wholesale corporate polo shirts requires navigating complex technical parameters—ranging from textile fiber physics and yarn twist densities to colorfastness thresholds and ethical compliance frameworks.
As a leading ISO 9001:2015 certified apparel manufacturer based in Gurgaon, India, Vihaan International operates at the nexus of technical textile engineering and agile contract manufacturing. This technical guide outlines the critical operational benchmarks, material engineering standards, and global procurement trends that procurement directors, brand directors, and supply chain managers must master when evaluating OEM (Original Equipment Manufacturer) and ODM (Original Design Manufacturer) polo shirt factories.
Material Specification & Fabric Performance Benchmark
Selecting the optimal fabric composition is the cornerstone of successful corporate uniform manufacturing. OEM procurement requires balancing tactile comfort, thermal regulation, wrinkle resistance, and print/embroidery receptivity.
| Fabric Composition | GSM Range | Piqué / Weave Structure | Key Performance Traits | Optimal Industry Application |
|---|---|---|---|---|
| 100% Combed Ring-Spun Cotton | 180 – 240 GSM | Classic Honeycomb Piqué | Ultra-soft touch, high breathability, premium natural drape | Executive Boardwear, Tech Management, Luxury Retail |
| CVC Blend (60% Cotton / 40% Poly) | 190 – 220 GSM | Double-Knit Micro Piqué | High tensile strength, minimal shrinkage (<3%), colorfast | Corporate Offices, Financial Institutions, Airline Staff |
| TC Blend (65% Poly / 35% Cotton) | 200 – 230 GSM | Heavy Duty Piqué / Interlock | Maximum abrasion resistance, quick drying, budget efficient | Hospitality Housekeeping, Warehouse Logistics, Maintenance |
| Performance Poly-Spandex (92/8) | 160 – 190 GSM | Moisture-Wicking Jersey / Birdseye | 4-way stretch, UPF 50+ protection, anti-microbial finish | Outdoor Operations, Golf & Sports Clubs, Delivery Services |
| Mercerized Supima Cotton | 160 – 200 GSM | Fine Gauge Flat Knit | Silk-like luster, zero surface fuzz, superior dye saturation | VIP Front Desk, Luxury Resort Concierge, C-Suite Uniforms |
Collar Engineering
Preventing "curl collar" is a hallmark of premium OEM manufacturing. We utilize fused interlinings and jacquard rib-knits with elastane yarns to guarantee collar shape retention after repeated washings.
Colorfastness Standards
All fabric lots undergo ISO 105-C06 washing tests and ISO 105-B02 light exposure testing, achieving Grade 4-5 color stability against UV degradation and industrial laundering detergents.
Precision Branding
Using Japanese Tajima multi-head embroidery machinery and high-density screen/sublimation printing, we achieve exact Pantone match (PMS) compliance down to 0.5mm logo detail.
5-Stage Quality Engineering & Contract Manufacturing Workflow
To eliminate defect risks in multi-thousand unit wholesale shipments, Vihaan International enforces a closed-loop quality control system compliant with international AQL 2.5 (Acceptable Quality Limit) benchmarks.
Future Global Sourcing Trends in Corporate Polo Apparel
1. Sustainable Eco-Yarns & Recycled Fibers
Global ESG mandates are driving enterprise procurement teams to transition from standard virgin polyester to GRS-certified (Global Recycled Standard) rPET recycled polyester and Organic Oeko-Tex Standard 100 cotton. Corporate buyers are utilizing lifecycle assessment (LCA) data to prove carbon footprint reductions in their annual sustainability reports.
2. Smart Functional Surface Treatments
The post-pandemic workforce demands hybrid performance apparel. Enterprise polo shirts are increasingly engineered with dual-action technology: moisture-wicking capillary channels on the interior coupled with hydrophobic stain-release coatings on the exterior, keeping staff clean and dry throughout 12-hour shifts.
3. "India+1" Supply Chain Diversification
As global brands mitigate geographic concentration risks, India has surfaced as the premiere destination for high-value apparel manufacturing. With vertical raw material access (world’s largest cotton producer), duty-advantaged trade agreements, and advanced OEM apparel clusters in Gurgaon/Delhi NCR, Indian suppliers provide unrivaled price-to-quality ratios.
4. Micro-MOQ On-Demand Replenishment
Traditional 5,000-unit minimum order quantities are giving way to agile matrix manufacturing. Leading OEM factories now support initial batch runs of 200–500 units per style with rapid digital re-ordering capability, allowing corporate clients to onboard new employees seamlessly without keeping excessive inventory.
Corporate Polo Shirt Design & Styling Innovations
The corporate polo shirt has stepped into the space between casual streetwear and structured business formal. Key architectural enhancements defining current production orders include:
Seamless Placket Construction
Replacing traditional visible stitch plackets with laser-cut bonded plackets and concealed magnetic or matte snap closures for a sleek, contemporary tech-company aesthetic.
Bio-Washing & Silicone Finish
Enzymatic bio-wash treatments remove surface micro-fibrils, producing a peach-skin softness and preventing fabric pilling even after prolonged friction and wear.
Ergonomic Underarm Gussets
Incorporating breathable 3D stretch mesh panels into underarm zones to enhance mobility and air circulation for active service personnel and field teams.
Why Enterprise Buyers Choose Vihaan International
Headquartered in Gurgaon, Haryana (India's premier industrial hub), Vihaan International combines state-of-the-art production infrastructure with direct export compliance to deliver seamless wholesale solutions.
Modern Industrial Facility
Located at 116 MA Tower, Udyog Vihar Phase 4, Gurgaon. Equipped with Juki automated sewing lines, computer pattern plotters, and dedicated QC bays capable of producing 20,000+ units monthly.
Turnkey Global Export
IEC-registered and DGFT-compliant. We export directly to USA, UK, Canada, France, EU, and Middle East under FOB, CIF, and DDP terms with complete shipping documentation.
Full Customization (OEM/ODM)
From Tech-Packs and custom Pantone yarn dyeing to branded neck tapes, woven size labels, hangtags, and individual eco-polybag packaging.
Frequently Asked Questions (B2B Procurement FAQ)
Answers to common operational questions regarding custom polo shirt orders, factory sampling, MOQs, and export logistics.
Partner With India's Leading Corporate Uniform Manufacturer
Scale your corporate apparel procurement with guaranteed quality, AQL 2.5 standards, and direct factory-gate pricing. Talk to our garment engineering team today.