Featured Commercial F&B Workwear & Hospitality Uniforms
Precision-stitched, industrial-launderable OEM/ODM aprons and professional service apparel tailored for global procurement standards.
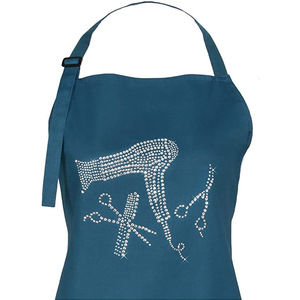
Baking Accessories Chef Apron Custom Logo Sublimation Women Eco-friendly Comfort Aprons
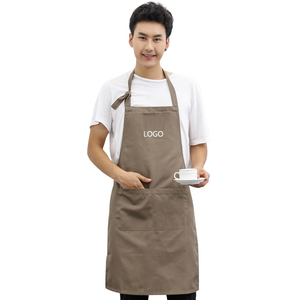
Kitchen Cleaning Multi-Function Durable Canvas Sleeveless Bib Apron With Utility Pockets
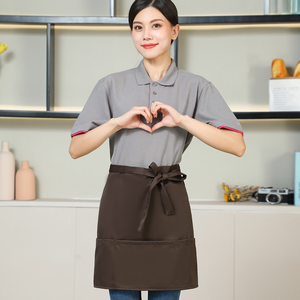
Fashion-Forward 5-Pocket Short Waist Apron Waterproof Reusable Polyester Retail/F&B Apron
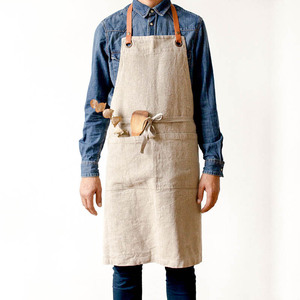
Kitchen Cotton Custom Logo Chef Durable Japanese Minimalist Style Cooking Aprons
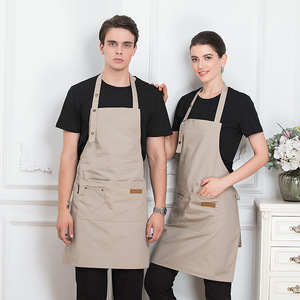
Custom Logo Premium Adjustable Cross-Back Canvas Work Apron for Baristas & Bakeries
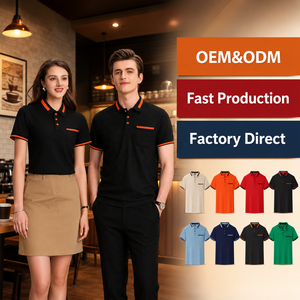
Wholesale Restaurant Hotel Front Desk Polo Shirts Custom Logo Server Waitstaff Uniforms
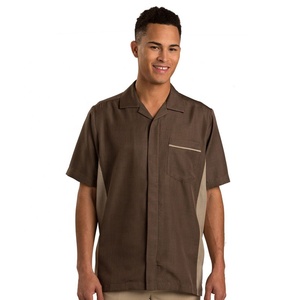
Customized Men's Short Sleeve Hotel Staff & Housekeeping Service Cleaning Uniform Shirts
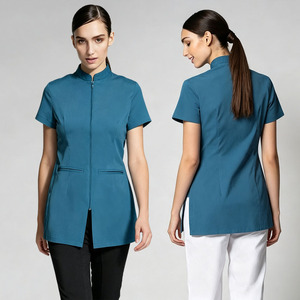
Custom Workwear Beauty Salon Spa & Hotel Hospitality Female Woven Luxury Uniform Scrubs
01. Executive Whitepaper: The Strategic Evolution of F&B Uniform Procurement
In the modern international Food & Beverage (F&B) and hospitality ecosystem, workwear is no longer treated as a passive operational expense. Instead, procurement directors, global franchise operators, and retail apparel brand buyers view custom aprons and staff uniforms as pivotal touchpoints for brand identity, ergonomic safety, and operational longevity. As a premier global OEM/ODM custom F&B aprons wholesale exporter operating out of Gurgaon, Delhi NCR, Vihaan International bridges the gap between high-volume garment manufacturing and precise textile engineering.
Global supply chains demand suppliers capable of fulfilling rigorous Original Equipment Manufacturing (OEM) and Original Design Manufacturing (ODM) requirements. From heat-resistant, grease-repellent chef aprons to fashion-forward 5-pocket waist aprons for fast-casual dining chains, the requirements of international buyers extend beyond simple aesthetic appeal. Modern aprons must withstand heavy-duty commercial laundering cycles (exceeding 60°C wash cycles), offer stain-release barrier technologies, incorporate ergonomic weight-distribution harnesses, and reflect strict sustainability compliance standardizations (OEKO-TEX Standard 100 and GOTS-certified organic cotton blends).
Core OEM/ODM Customization Capabilities
Exhaustive textile modification, reinforcement options, and custom branding protocols designed for enterprise supply chains.
Advanced Liquid & Stain Barriers
Integration of C0 fluorocarbon-free hydrophobic coatings and Teflon™ soil-release finishes ensuring resistance against hot oils, sauces, and harsh kitchen chemicals without compromising fabric breathability.
Ergonomic Weight Distribution
Custom cross-back (X-back) webbing systems, adjustable genuine/vegan leather harnesses, and padded shoulder supports designed to alleviate neck strain during 12-hour commercial kitchen shifts.
Structural Bar-Tack Reinforcement
High-stress points—including pocket corners, strap joinery, and towel loop anchor points—undergo heavy-duty 28-stitch bar-tack reinforcement to withstand continuous mechanical friction.
02. Technical Fabric Performance & Material Selection Matrix
Choosing the correct textile blend is the foundational decision in commercial workwear procurement. Below is a comparative technical analysis of fabric substrates utilized in our OEM/ODM custom F&B apron manufacturing lines:
| Fabric Blend / Substrate | Weight (GSM) | Commercial Launderability | Tensile Strength | Best Application Scenario |
|---|---|---|---|---|
| 65/35 Poly-Cotton Twill | 220 – 240 GSM | Excellent (60°C+ Industrial) | High (Colorfast) | High-volume restaurant chains, server bib aprons, prep cooks |
| 100% Heavyweight Cotton Canvas | 280 – 340 GSM | Good (Natural Wear) | Ultra-High (Abrasion Proof) | Artisanal bakeries, specialty coffee barista aprons, craft breweries |
| Hydrophobic Polyester Ripstop | 180 – 210 GSM | Superior (Fast Dry) | Maximum (Tear Proof) | Dishwashing stations, meat processing, industrial kitchen cleaning |
| Recycled PET (rPET) Blend | 200 – 230 GSM | High (Sustainable) | High (Eco-Compliant) | ESG-focused hotel groups, eco-conscious retail brands, organic cafes |
03. Global Procurement Trends & Future Market Dynamics (2025–2030)
As enterprise procurement managers navigate evolving global trade shifts, several macro trends are defining the future of F&B uniform and apron sourcing:
1. Shift Toward Supply Chain Resiliency & India Sourcing: Global brands are increasingly adopting a "China+1" diversification model. India's robust vertical integration in textiles—spanning raw cotton production, advanced spinning mills, and skilled garment manufacturing—makes it the preferred destination for high-reliability apparel exports. Facilities in major industrial hubs like Gurgaon, Delhi NCR provide seamless connectivity to international ports and airports, ensuring predictable lead times.
2. Strict Regulatory & Chemical Compliance (PFAS-Free Mandates): Statutory bodies in North America (US FDA/EPA) and Europe (EU REACH) are aggressively phasing out per- and polyfluoroalkyl substances (PFAS) in textile finishes. Forward-thinking F&B exporters must offer certified PFAS-free, water- and oil-repellent alternatives that achieve water column ratings without hazardous fluorocarbons.
3. Modular & Gender-Neutral Pattern Design: Modern hospitality workwear is shifting away from rigid gender-specific cuts toward adjustable, unisex modular patterns. Incorporating multi-position snap button neck straps, removable cross-back harnesses, and dynamic waist sliders reduces SKU complexity for corporate buyers by 35%, allowing a single apron model to comfortably fit diverse workforce demographics.
OEM Manufacturing Protocol
Ideal for established corporate brands with complete Tech Packs. We execute client-provided tech specifications, exact CAD pattern cutting, Pantone-matched custom dyeing, precise logo embroidery/screen printing, and custom hardware trim sourcing with absolute secrecy under NDA protection.
ODM Turnkey Product Creation
Designed for growing hospitality chains and private label importers seeking market-ready design engineering. Our in-house design team provides pre-tested apron silhouettes, material recommendations, functional pocket layout design, and quick-turn prototyping to accelerate your product launch.
04. Vihaan International: Manufacturing Infrastructure & Quality Excellence
Headquartered in Gurgaon, Haryana (India), Vihaan International is an ISO 9001:2015 certified manufacturer and exporter of corporate apparel, hotel uniforms, and custom F&B workwear. Operating with a robust monthly production capability exceeding 20,000+ completed garment units, our facility integrates Japanese industrial JUKI stitching units, automated CAD pattern-grading plotters, and specialized branding lines.
Our export infrastructure holds active Import Export Code (IEC) registrations and operates in strict compliance with the Directorate General of Foreign Trade (DGFT), Government of India. We regularly service enterprise clients, luxury 5-star hotel chains, restaurant groups, and fashion importers across the United States, United Kingdom, Canada, France, European Union, and the Middle East (UAE, Saudi Arabia, Qatar). All international orders are supported under flexible Incoterms including FOB, CIF, and DDP (Delivered Duty Paid).
The 5-Stage AQL 2.5 Quality Assurance Framework:
Every batch of OEM/ODM aprons passes through an uncompromised 5-checkpoint quality control workflow:
- Stage 1: Raw Material Inspection: GSM measurement, dimensional shrinkage testing, color fastness to rubbing and commercial washing.
- Stage 2: CAD Pattern & Precision Cutting: Computerized lay-planning to guarantee zero grain-line distortion and consistent garment sizing across bulk lots.
- Stage 3: In-Line Stitching Audit: Continuous monitoring of stitch density (12–14 stitches per inch), seam tension, and bar-tack placement every 3rd operation.
- Stage 4: Logo & Branding QC: High-density embroidery stitch count checks, sublimation heat-transfer wash durability, and metallic rivet stress testing.
- Stage 5: Pre-Shipment AQL Inspection: 100% thread trimming, iron pressing, folding, polybag packaging, and carton drop testing compliant with AQL Level II standards.
Frequently Asked Questions (FAQ) for Global Buyers
Detailed technical and logistical answers to help procurement officers and sourcing managers make informed supplier decisions.