Featured Healthcare & Medical Staff Apparel
Direct-from-factory wholesale scrub tops, clinical uniforms, and multi-department healthcare workwear customized to exact hospital specifications.
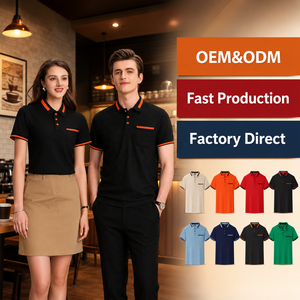
Wholesale Custom Hospital & Clinical Staff Polo Shirt Uniforms
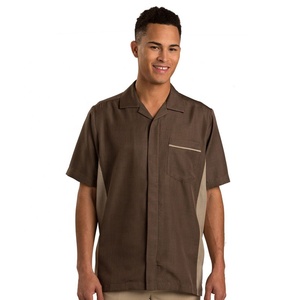
Short Sleeve Clinical Nurse & Housekeeping Scrub Shirt
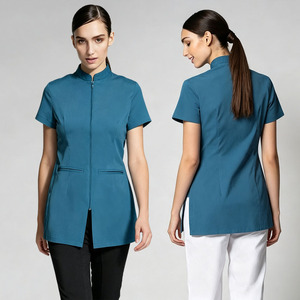
Custom Woven Ergonomic Female Nurse & Spa Scrubs Suit
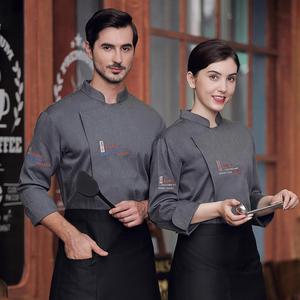
Long Sleeve Anti-Fluid Hospital Kitchen & Sanitization Uniform
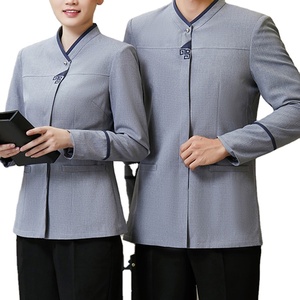
Unisex Hospital Support Staff & Housekeeping Workwear Jacket
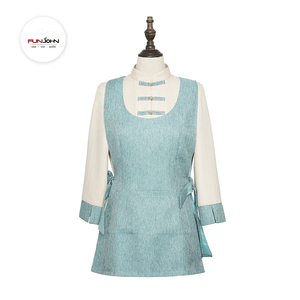
Women's 2-Piece Long Sleeve Hospital Service & Duty Uniform
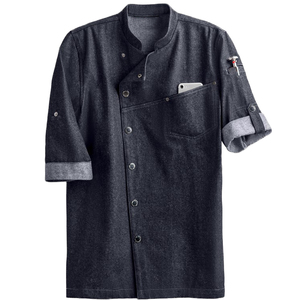
Custom Heavy-Duty Hospital Duty & Maintenance Staff Jacket
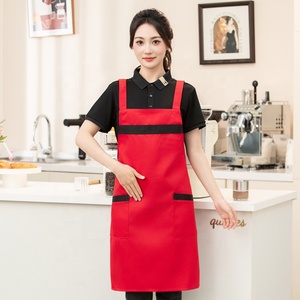
Hospital Catering & Hygiene Protection Apron Workwear
Executive Whitepaper: Strategic Sourcing for Hospital Nurse Uniforms
The global healthcare textile market is undergoing a paradigm shift. Modern hospital procurement directors and healthcare facility administrators no longer treat medical scrubs and nurse uniforms as mere operational commodities. Instead, nursing apparel is recognized as a vital component of infection prevention, personnel ergonomics, brand identity, and employee retention strategies. As an ISO 9001:2015 certified OEM manufacturer, Vihaan International provides deep technical insights into custom medical apparel manufacturing, raw material science, and global procurement optimization.
The Paradigm Shift in Medical Uniform Engineering
Historically, standard hospital scrubs relied on basic 100% heavy cotton or low-grade polyester-cotton weaves that suffered from severe color fading after high-temperature commercial laundering, excessive fabric stiffness, and lack of fluid barrier protection. Today's healthcare environments—spanning intensive care units (ICUs), emergency departments, surgical suites, and outpatient clinics—demand high-performance hybrid fabrics. Modern nurse uniforms must offer 4-way mechanical stretch, moisture-wicking capillary technology, fluid-repellent DWR (Durable Water Repellent) coatings, and antimicrobial silver-ion treatments that neutralize nosocomial pathogens.
Furthermore, ergonomics plays a critical role in clinical efficiency. Registered Nurses (RNs) and Nurse Practitioners (NPs) execute physical tasks including patient transfers, prolonged standing, and rapid clinical movements during 12-hour shifts. Apparel designed without anatomical gusseting, reinforced stress-point bar-tacking, or flexible waistband construction leads to premature garment degradation, reduced range of motion, and physical fatigue.
Technical Fabric Engineering Matrix for OEM Hospital Apparel
Our facility in Gurgaon, Delhi NCR utilizes specialized textile blends tailored to distinct hospital departments. Below is our engineering benchmark for bulk manufacturing:
| Fabric Grade | Composition & Weight | Performance Characteristics | Departmental Suitability | Laundering Tolerance |
|---|---|---|---|---|
| Pro-Flex Spandex Blend | 72% Poly / 21% Rayon / 7% Spandex (180 GSM) | 4-Way Stretch, Ultra-Soft Touch, Moisture Wicking, Anti-Wrinkle | ICU, ER, Surgical Nurses, Pediatrics | Industrial wash up to 60°C |
| Shield-Tech Anti-Microbial | 65% Poly / 35% Cotton + Silver Ion (200 GSM) | Bacterial Barrier, Fluid Repellent, Fade-Resistant Vat Dyed | Infectious Disease Ward, General Nursing | High-Temp Sterilization 75°C+ |
| Eco-Tech Recycled PET | 60% rPET / 35% Organic Cotton / 5% Elastane (175 GSM) | Sustainable Sourcing, Breathable, Lightweight, Odor Resistant | Outpatient Clinics, Wellness & Rehab | Standard Commercial Laundering |
| Heavy-Duty Utility Canvas | 65% Polyester / 35% Cotton Twill (240 GSM) | Abrasion-Resistant, Reinforced Tensile Strength, Stain-Release | Hospital Facility Maintenance, Sanitation | Heavy Industrial Wash & Autoclave |
Future Procurement Trends for Hospital Nurse Uniforms
Key shifts impacting global B2B procurement, supply chain diversification, and hospital tender specifications over the next decade.
1. Pathogen-Shield Smart Textiles
Hospital procurement tenders increasingly mandate permanent antibacterial and antiviral fabric finishes. Future contracts require silver-ion, copper-oxide, or silane quaternary ammonium salt treatments integrated at the yarn level rather than topical coatings, ensuring efficacy through 100+ commercial wash cycles.
2. Closed-Loop Circular Recycled Blends
ESG (Environmental, Social, and Governance) compliance has moved to the forefront of hospital group purchasing organizations (GPOs). Procurement managers are shifting toward recycled polyester (rPET) derived from post-consumer plastic bottles, reducing scope 3 carbon emissions without sacrificing tensile strength.
3. Color-Coded Departmental Systems
To streamline emergency response and patient clarity, major hospital networks are adopting strict color-coded uniform standards (e.g., Royal Blue for Registered Nurses, Ceil Blue for Surgical Techs, Charcoal for Radiology). Factories must deliver precise Pantone color consistency across batch re-orders.
4. Multi-Hub OEM Manufacturing
Global healthcare brands are diversifying manufacturing outside single-source regions to prevent supply line chokepoints. India, with its robust vertical cotton integration and advanced synthetic textile manufacturing hubs in NCR and Gujarat, has emerged as the premier OEM partner for Western healthcare buyers.
5. Athletic-Inspired Ergonomic Cuts
The boundary between technical sportswear and medical apparel has dissolved. Modern nurse uniform designs feature jogger-style pants with elastic rib cuffs, athletic waistband drawstrings, multi-functional utility cargo pockets, and side mesh venting panels for maximum airflow.
6. Digitalized Customization & RFID
Enterprise hospital clients are integrating heat-sealed UHF RFID chips into uniform hems for automated laundry sorting, inventory tracking, and loss prevention. OEM factories must offer precision RFID patch insertion and micro-embroidery branding directly during cut-and-sew operations.
Future Development Trends for Healthcare Apparel Garment Factories
To stay competitive, apparel manufacturing plants are transforming into smart factories. Below are the technological developments reshaping the OEM/ODM landscape for hospital nurse uniform manufacturing:
- Automated CAD Pattern Grading & Laser Cutting: Elimination of manual cutting errors through computer-aided pattern nesting, maximizing fabric utilization and achieving zero-tolerance seam accuracy across sizes XS to 5XL.
- Programmable Automatic Sewing Stations: Integration of automated JUKI pocket-setting machines, automatic sleeve-attaching units, and computerized bar-tackers to guarantee uniform seam strength at stress points.
- Digital Twin Prototyping: Utilizing 3D garment simulation software (CLO 3D / Optitex) to provide international buyers with virtual sample fitting within 48 hours, reducing physical sample iteration time by 70%.
- Traceable Supply Chains & GOTS / GRS Compliance: Establishing full chain-of-custody tracking from raw yarn spinners to finished garment packaging, supporting Global Recycled Standard (GRS) and Oeko-Tex Standard 100 certifications.
Vihaan International: Premier OEM Hospital Apparel Manufacturer
Headquartered in Gurgaon, Delhi NCR, India, we combine state-of-the-art machinery with ethical manufacturing to supply global enterprises, hospital networks, and private label apparel brands.
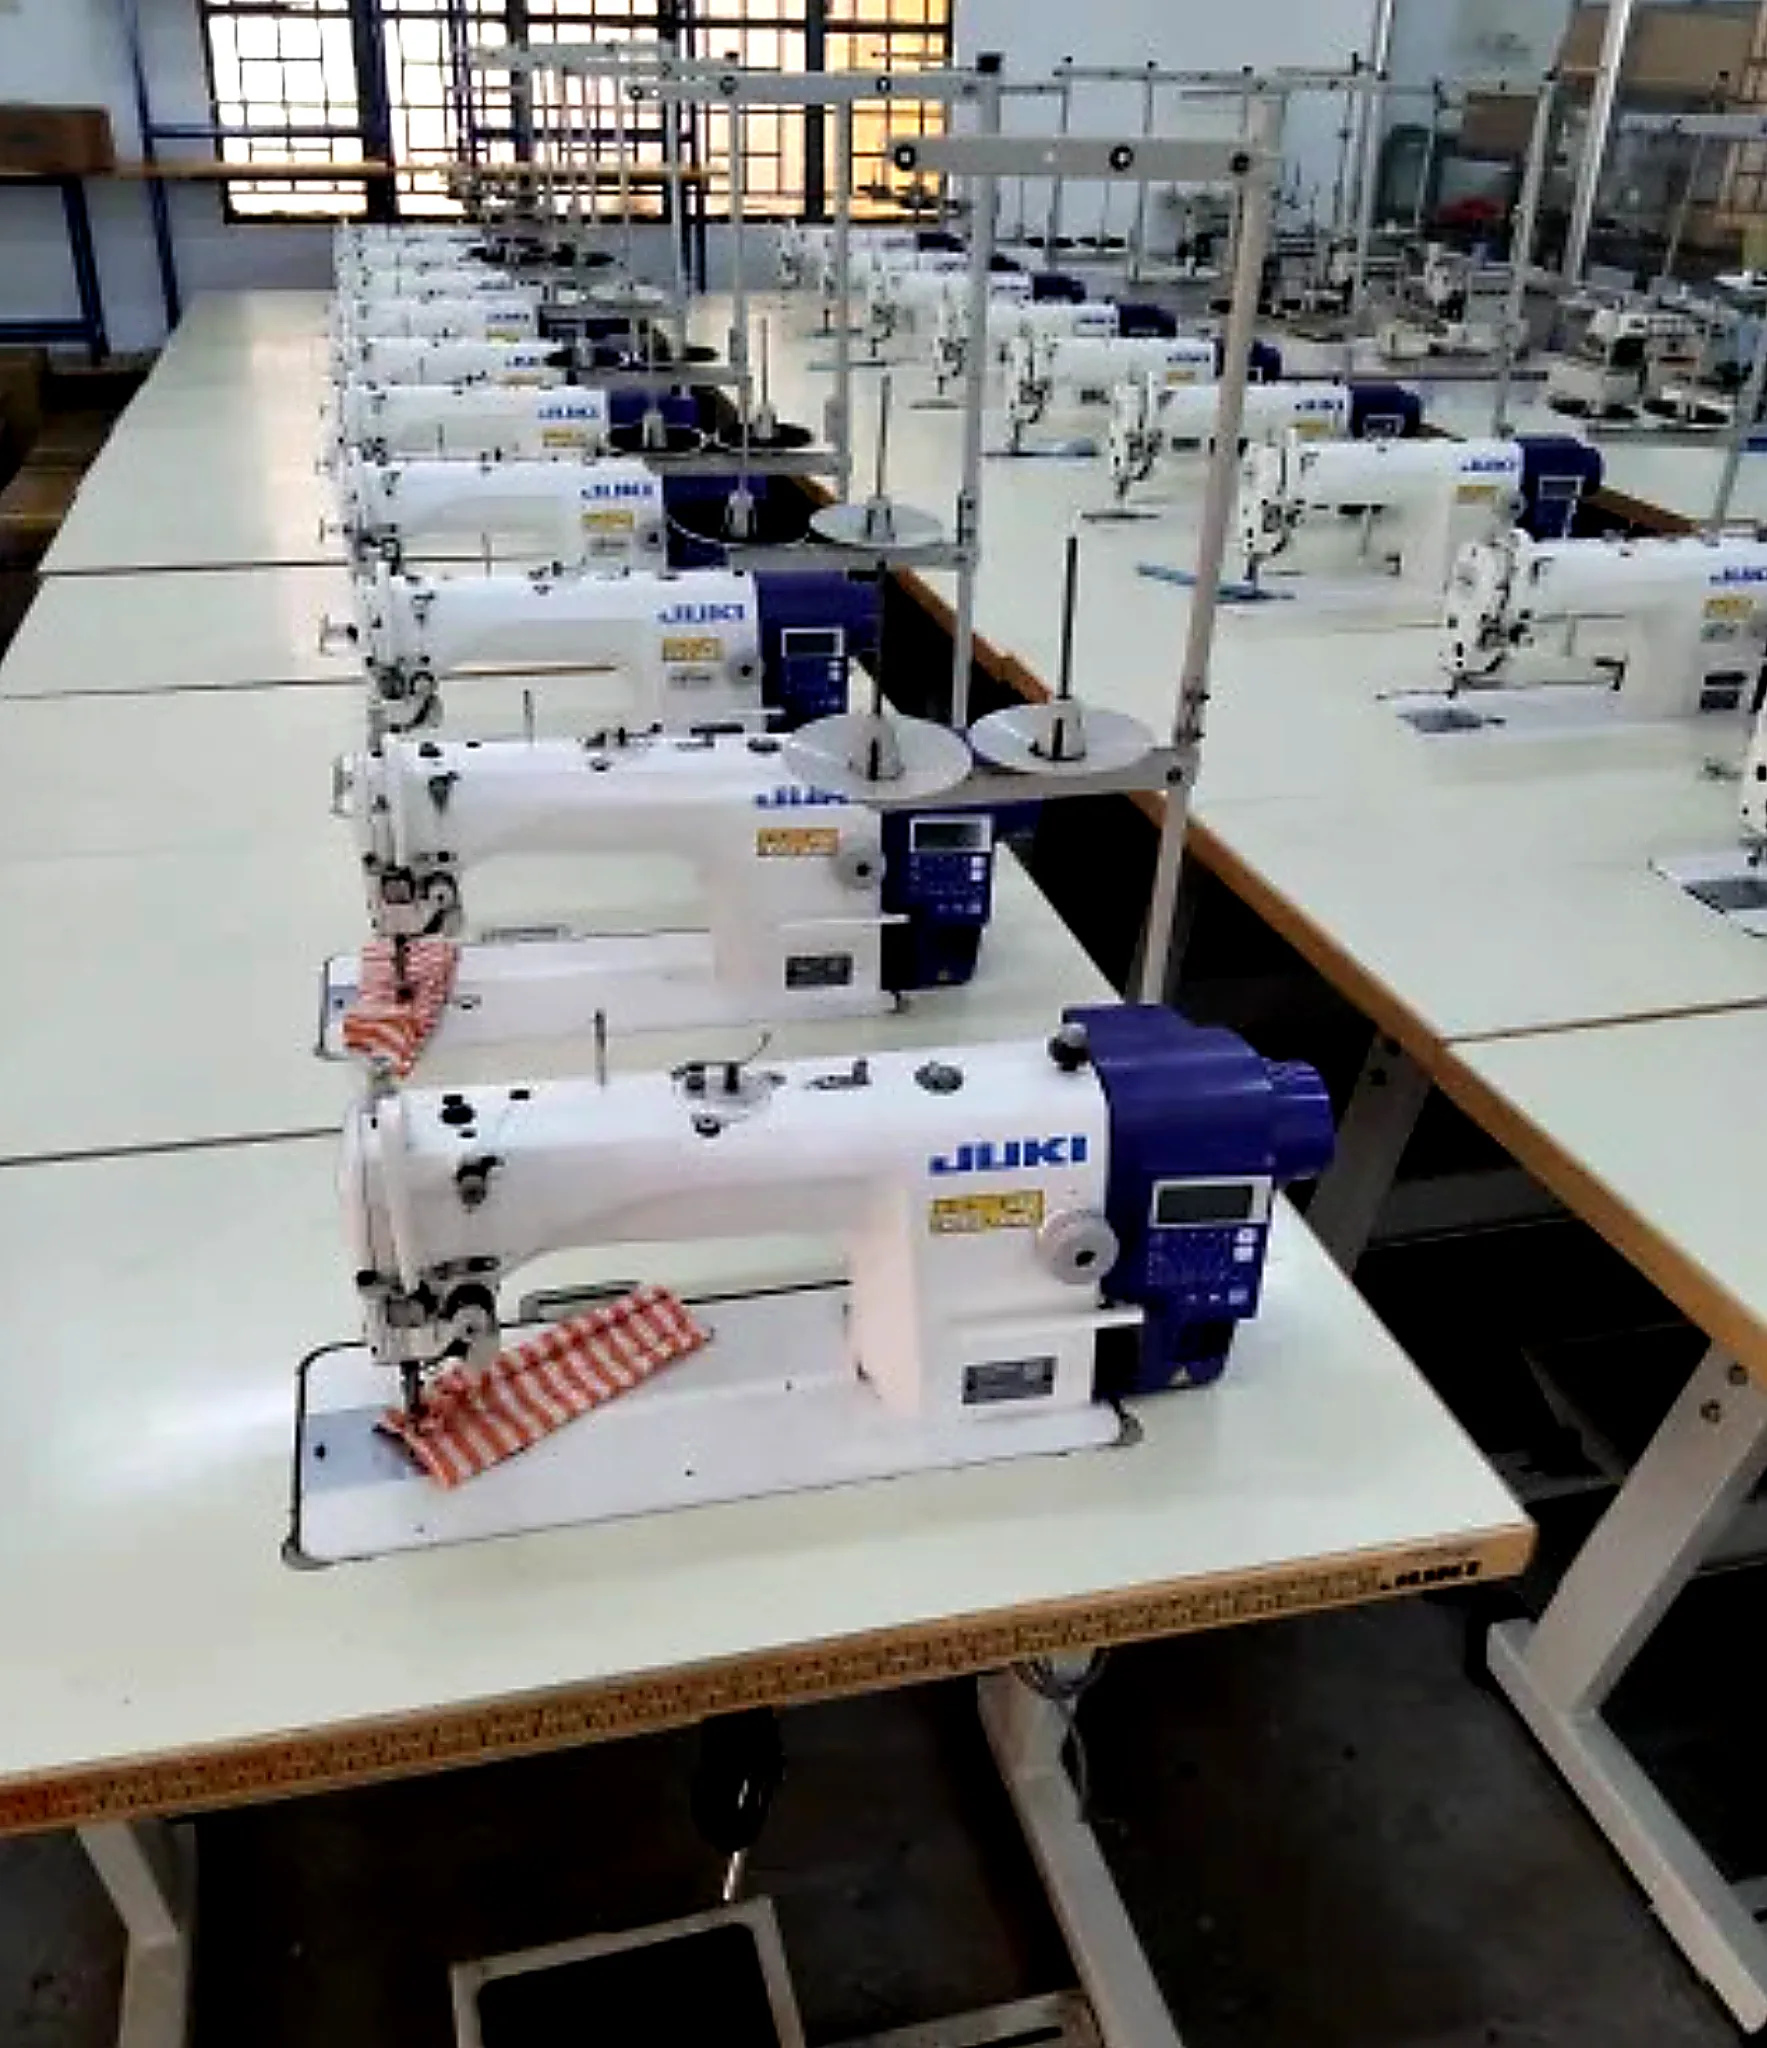
Manufacturing Infrastructure Built for Scale
Operating a fully integrated facility in Gurgaon, India, Vihaan International houses over 50+ skilled garment technicians and high-speed Japanese industrial sewing machinery (JUKI, Brother). We manage dedicated production lines for corporate apparel, hospitality uniforms, and medical scrubs.
- Production Capacity: 20,000+ units per month with scalable shift adjustments for rush contracts.
- ISO 9001:2015 Certified: Standardized Operating Procedures (SOPs) governing pattern making, cutting, stitching, and finishing.
- Export Infrastructure: Registered IEC (Import Export Code) and DGFT compliant, routinely shipping FOB, CIF, and DDP terms to USA, UK, EU, Canada, and UAE.
- Flexible MOQs: Support for enterprise buyers (5,000+ units/PO) as well as boutique private label launches (from 200–500 units/style).
5-Stage AQL 2.5 Quality Control Assurance
4-Point System fabric testing for GSM, colorfastness against chlorine, shrinkage rate, and tensile strength.
Precision automated cutting verified against approved size charts to prevent sizing variance across production batches.
Quality supervisors check stitch density (SPI 10-12), pocket placement, sleeve alignment, and bar-tack tension during assembly.
Embroidery tension, high-density screen printing durability, button lock-stitching, and thread trimming evaluation.
100% individual garment pressing, polybag insertion, carton drop-testing, and formal AQL 2.5 audit report release.
Hospital Uniform Procurement FAQs
Detailed technical answers to common queries raised by international buyers, medical distributors, and facility managers.
Q1: What is the Minimum Order Quantity (MOQ) for custom OEM nurse uniforms?
Our standard MOQ for custom OEM hospital nurse uniforms and medical scrub suits starts at 500 units per style/colorway for custom dyed fabrics. However, for private label brands or clients utilizing our standard stocked fabric colors (e.g., Ceil Blue, Navy Blue, Royal Blue, Black, Wine Red), we can accommodate trial orders starting from 200 units.
Q2: Can you manufacture uniforms according to custom hospital Pantone color standards?
Yes. We provide complete laboratory dip (lab-dip) color matching according to the Pantone Fashion, Home + Interiors (TCX/TPG) color system. Lab dips are submitted within 5–7 working days for client spectrophotometer approval prior to bulk fabric dyeing.
Q3: How do your nurse uniforms withstand intensive commercial laundry sterilization?
We use high-tenacity polyester sewing threads, vat-dyed colorfast fabrics, and reinforced double-needle cover-stitching. Our fabrics are lab-tested to withstand industrial laundering cycles up to 75°C (167°F) and chlorine bleaching protocols without color fading or seam degradation.
Q4: What branding techniques do you offer for hospital logo integration?
We offer multi-head computer embroidery (up to 15 colors), high-density silk screen printing, silicone heat transfer logos, woven brand labels, and laser-engraved buttons. Custom emergency contact tags, RFID tracking patches, and individual employee name embroideries are also available.
Q5: What are the typical sample lead times and bulk production turnaround times?
Standard pre-production physical samples are delivered in 7 to 10 days. Upon sample sign-off and deposit confirmation, bulk production turnaround takes 15 to 25 days depending on order volume and fabric customization specifications. Air freight and ocean freight logistic options are fully managed by our export desk.
Q6: Do you provide custom sizing and gender-specific ergonomic patterns?
Yes, we offer separate female-tailored, male-tailored, and unisex fit patterns. Our sizing charts align with US, UK, EU, and Middle Eastern size metrics (ranging from XXS to 5XL), featuring contoured waistlines, chest darts, multi-pocket utility placements, and adjustable side vents.
Partner With a Trusted OEM Medical Uniform Factory
Request a direct factory price quotation, request fabric swatch cards, or speak with our garment technical specialists today.