Featured Healthcare & Institutional Workwear Collections
High-performance hospital apparel engineered for ergonomic comfort, high-temperature industrial laundering, and superior fluid repellency.
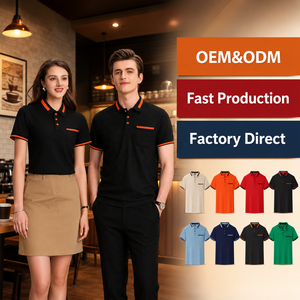
Wholesale Medical & Healthcare Staff Polo Shirts with Custom Printed Logo
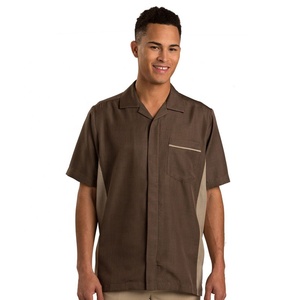
Customized Men's & Women's Short Sleeve Hospital Nurse Scrub Shirt
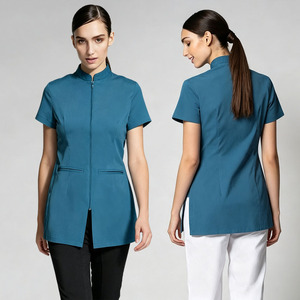
Custom Clinical Work Wear & Medical Spa Female Uniform Scrubs Set
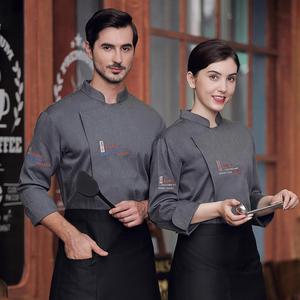
Wholesale Hospital Dietary & Kitchen Chef Uniform Long Sleeves
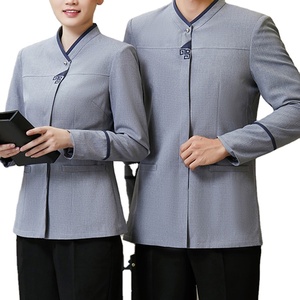
Unisex Hospital Sanitization & Housekeeping Service Jacket Uniform
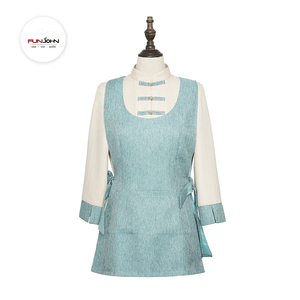
Women's 2pcs Long Sleeve 100% Polyester Hospital Administrative Uniform
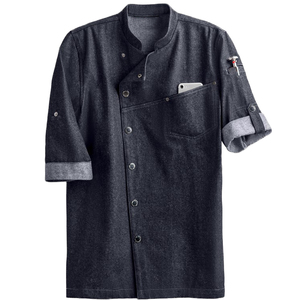
Custom Denim Work Jacket Uniform for Medical Facility Maintenance Staff
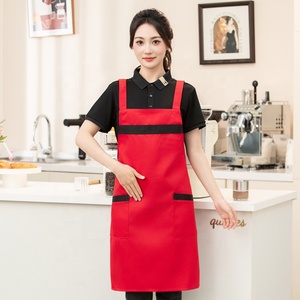
Professional Healthcare Laboratory & Catering Protective Aprons Unisex
Executive Sourcing Guide: China Wholesale Healthcare Uniform Manufacturing
A comprehensive evaluation framework for hospital procurement directors, medical apparel wholesalers, and global healthcare brand importers.
As a leading China Wholesale Healthcare Uniforms Manufacturer & Exporter, our manufacturing infrastructure is purpose-built to address the complex requirements of modern healthcare systems worldwide. Medical workwear procurement has transitioned from standard garment sourcing to high-precision technical textile engineering. Today’s hospitals, outpatient clinics, emergency centers, and dental networks demand apparel that combines medical-grade barrier protection, ergonomic compliance, and high-frequency industrial wash endurance.
Operating from our integrated manufacturing facilities with over 20,000 units monthly capacity, we engineer medical apparel that complies with global standards including EN ISO 13795, AAMI PB70 fluid barrier specs, and ISO 9001:2015 quality management systems. From antimicrobial surgical scrubs to fluid-resistant lab coats and patient care gowns, our export division provides full OEM/ODM private-label manufacturing for enterprise buyers across North America, Europe, the Middle East, and Australia.
Enterprise Manufacturing Advantages
Why Tier-1 medical supply distributors and healthcare chains partner with our manufacturing facility.
Antimicrobial Fabric Engineering
Integration of Silver-Ion (Ag+) and Silvadur™ technologies into woven and knit fibers, preventing 99.4% of bacterial growth, cross-contamination, and odor generation across 100+ wash cycles.
Industrial Laundry Durability
Engineered using high-tenacity polyester staple fibers combined with long-staple combed cotton, designed to withstand continuous commercial laundering at 75°C (167°F) without color fading or fabric shrinkage.
Ergonomic 4-Way Stretch
Incorporating 3% to 7% Spandex / Elastane into high-stress scrub zones, allowing 360-degree range of motion for surgeons, nurses, and emergency medical technicians during 12-hour shifts.
5-Stage Quality Control Protocol
Every lot undergoes stringent AQL 1.5/2.5 testing: raw fabric GSM audit, seam tensile strength checks, fluid penetration barrier tests, embroidery colorfastness, and final sterile packaging inspection.
Full Global Export Compliance
Registered exporter with complete customs documentation, CE certification, FDA listing support, REACH chemical compliance, and flexible shipping terms (FOB, CIF, DDP) to over 15 countries.
Private Label & OEM/ODM Flexibility
Custom hospital brand execution including woven neck labels, RFID laundry chip installation, custom Pantone dyeing, contrast piping, and department-specific color coding.
Future Procurement Trends in Healthcare Uniform Sourcing (2025–2030)
The global healthcare apparel market is experiencing a structural shift driven by advanced material science, hospital sustainability mandates, and digital inventory tracking. Sourcing officers must evaluate the following key trends when structuring long-term procurement contracts with Chinese manufacturing partners:
- Integration of UHF RFID Tracking Chips: Modern medical facilities are transitioning to automated linen and uniform management systems. Micro-encapsulated Ultra-High Frequency (UHF) RFID chips woven into neck seams allow automated tracking of garment wash cycles, inventory loss prevention, and life-cycle replacement alerts across commercial laundries.
- Sustainable Recycled Polyester (rPET) Blends: Leading hospital networks are adopting eco-friendly scrubs made from post-consumer recycled plastic bottles. Our rPET fabric lines reduce carbon emissions by 45% while matching the tensile strength and hand-feel of virgin polyester fibers.
- Advanced Liquid Barrier Technologies (AAMI Level 1-3): Moving away from heavy, un-breathable plastic coatings, modern scrubs utilize nanotech fluorocarbon-free water-repellent (DWR) finishes that cause blood, saline, and bodily fluids to bead up and roll off without compromising tissue breathability.
- Shift Toward Athleisure-Inspired Scrub Designs: Hospital staff increasingly prefer modern, tailored silhouettes featuring jogger scrub pants, ribbed ankle cuffs, utility zip pockets, and multi-directional stretch fabrics that blur the line between clinical uniforms and athletic performance wear.
Technical Fabric Comparison & Sourcing Specifications
Selecting the appropriate fabric composition is critical to optimizing garment lifespan, staff comfort, and cost-per-wear metrics. The table below outlines the core fabric specifications engineered in our manufacturing facility for global wholesale orders:
| Uniform Category | Fabric Composition | Weight (GSM) | Key Performance Feature | Target Healthcare Application |
|---|---|---|---|---|
| Premium Flex Scrubs | 72% Poly / 23% Rayon / 5% Spandex | 175 - 190 GSM | 4-Way Stretch, Moisture Wicking | Surgeons, ER Nurses, Private Clinics |
| Standard Hospital Scrubs | 65% Polyester / 35% Cotton Twill | 160 - 180 GSM | High Temp Washable, Chlorine Proof | General Hospital Staff, Ward Nurses |
| Barrier Lab Coats | 80% Polyester / 20% Cotton Poplin | 190 - 210 GSM | Fluid Repellent, Stain Release Finish | Physicians, Lab Technicians, Researchers |
| Patient Care Gowns | 50% Cotton / 50% Polyester Plain | 130 - 150 GSM | Soft Skin Feel, High Tear Resistance | Inpatient Wards, Rehabilitation Centers |
| Sanitization & Facility Wear | 100% Polyester Heavy Twill | 220 - 240 GSM | Abrasion Resistant, Quick Drying | Environmental Services, Maintenance |
Frequently Asked Questions (Sourcing FAQ)
Answers to common B2B procurement queries regarding minimum order quantities, customization, shipping, and quality assurance.
Partner with China's Premier Healthcare Garment Exporter
Get direct factory pricing, fabric swatches, and technical consultations for your hospital uniform or private-label medical collection.