High-Demand Custom Corporate & Hospitality Apparel
Explore our factory-direct custom workwear, hotel uniforms, and tactical staff wear engineered for durability, brand alignment, and scalable production.
1. Executive Analysis: The Shift in Global OEM Custom Apparel Sourcing
In the contemporary B2B procurement environment, selecting a supplier under the designation of China Top OEM Custom Apparel Production Manufacturers & Suppliers requires far more than basic price-per-piece evaluation. Modern international brands, hospitality conglomerates, corporate enterprises, and aviation lines demand integrated technical design capabilities, rigorous quality control frameworks, and total supply chain transparency.
The global textile and apparel industry has entered an era governed by Information Gain and Semantic Precision. B2B buyers no longer search for generic clothing factories; their search intent centers around specialized engineering parameters: technical fabric GSM (Grams per Square Meter), colorfastness to commercial laundering, seam tensile strength, flame-retardant finishes, and ISO-certified manufacturing compliance.
Technical CAD & Pattern Optimization
Our OEM operations leverage computerized CAD pattern-making to eliminate dimensional variances across bulk sizing runs. This ensures that a size Medium specified for North America matches international grading protocols with zero marginal deviation.
Material Matrix & Textile Sourcing
Direct integration with certified yarn spinners allows us to formulate custom fiber blends—including 100% combed long-staple cotton, poly-cotton high-density twill, anti-static synthetic weaves, and moisture-wicking bamboo viscose.
ISO 9001:2015 & Audit Readiness
Operating under strict Quality Management System (QMS) protocols, our production floors are optimized for third-party auditing standardizations including ISO 9001:2015, BSCI compliance, and DGFT/IEC international trade verification.
2. OEM Custom Apparel Technical Specifications & Standards
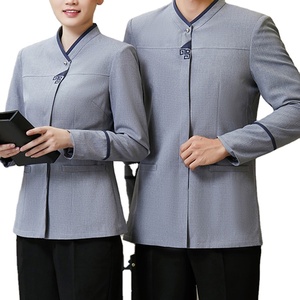
To ensure high performance across demanding commercial applications—such as luxury 5-star hotel front desks, intensive kitchen staff environments, and medical spas—every garment line undergoes standardized laboratory evaluation. Below is our engineering benchmark table for custom corporate and workwear manufacturing.
| Garment Category | Recommended Fabric Composition | Weight (GSM) | Colorfastness Rating | Specialty Finishing / Properties |
|---|---|---|---|---|
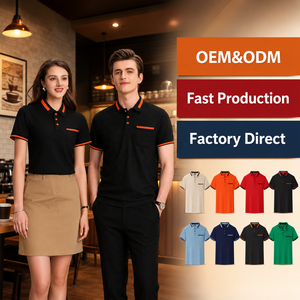
| Hospitality Polo Shirts | 65% Polyester / 35% Combed Cotton Piqué | 210 - 240 GSM | Grade 4.5 (ISO 105-C06) | Anti-Pilling, Mercerized, Reinforced Collar Stays |
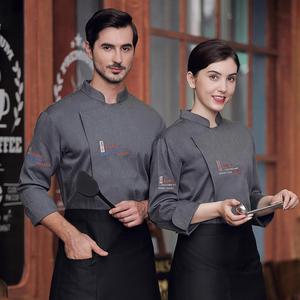
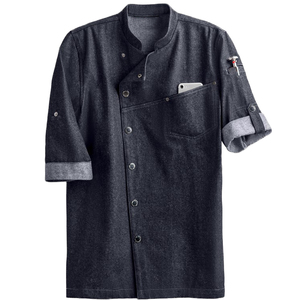
| Executive Chef Jackets | 100% Heavy-Duty Cotton Twill / Denim | 240 - 280 GSM | Grade 4.0 (Commercial Wash) | Heat Resistance, Stain-Repellent Nano-Coating |
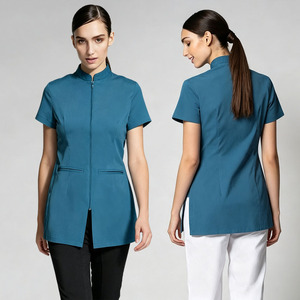
| Housekeeping & Spa Uniforms | 100% Microfiber Polyester or Poly-Rayon Blend | 160 - 190 GSM | Grade 4.2 (Perspiration/Light) | Breathable, Quick-Dry, Ergonomic Flex Stitching |
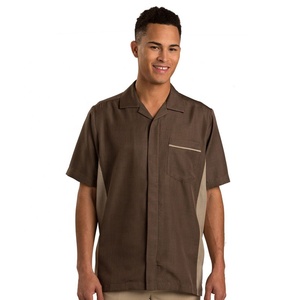
| Corporate Blazers & Workwear | Poly-Viscose Wool Touch Woven Structure | 280 - 340 GSM | Grade 4.5 (Dry Cleaning) | Wrinkle-Free Interlining, Anti-Static Lining |
By maintaining these quantifiable standards, our client partners eliminate sample mismatch and reduce customer return rates to near-zero levels during bulk distribution.
3. Future Procurement Trends in Custom Apparel Manufacturing (2026–2030)
As the apparel sourcing landscape evolves, B2B buyers must adapt to four pivotal shifts redefining OEM custom apparel production globally.
AI-Driven Tech-Pack Automation
Manual tech-pack interpretation is being superseded by digital twin pattern modeling. Automated parsing of vector garment files allows pattern engineers to generate grading charts in hours rather than days, drastically reducing pre-production lead times.
Circular & Recycled Synthetics
Global regulations are mandating higher percentages of rPET (Recycled Polyethylene Terephthalate) in corporate workwear. Leading OEMs now integrate GOTS-certified organic cotton and GRS-certified recycled polyester directly into standard uniform catalogs.
Agile Low-MOQ Batch Scaling
Enterprise clients are moving away from massive single-shipment inventory locks toward modular ordering. Modern OEM facilities utilize flexible assembly lines capable of economic runs starting at 200–500 units with fast re-order turnarounds.
Smart Workwear Integration
From embedded RFID chips for industrial uniform inventory management to anti-microbial silver-ion treatments for salon and airport personnel, functional technology integration is becoming a standard specification in corporate purchasing tenders.
4. Technological Innovations in OEM Garment Engineering
Achieving superior structural integrity and visual distinction in custom uniforms requires specialized machinery and modern assembly methodologies. Our factory infrastructure incorporates automated sewing units, multi-head computer embroidery systems, and precision heat-transfer sublimators.
Automated Fabric Spreading
Laser-guided laying machines ensure stress-free tension control prior to automated blade cutting.
High-Density Embroidery
Tajima multi-head digital embroidery machinery delivers crisp logo definition up to 12,000 stitches/min.
Seam Sealing & Reinforcement
Double-needle lockstitching and bar-tack reinforcements applied at all major stress points and pocket corners.
Screen & Sublimation Print
Eco-friendly plastisol and water-based inks offer high stretchability without cracking or fading after repeated washes.
AQL 2.5 Final Inspection
100% inline checking combined with final statistical sampling for thread trims, measurement tolerances, and packaging.
5. Corporate Advantages: Enterprise-Grade Apparel Manufacturing
Leveraging deep industrial experience, state-of-the-art production facilities, and an audited network of specialized textile partners, our corporate infrastructure delivers uncompromised reliability for international procurement teams.
Scalable Monthly Capacity (20,000+ Units)
Our dedicated production lines support continuous bulk production across polos, woven shirts, scrub tops, chef jackets, and structured blazers. We comfortably manage high-volume recurring enterprise orders with guaranteed line reservation.
7-Day Rapid Prototyping & Sampling
Accelerate your product launch timeline with our dedicated rapid-sample room. From vector artwork or physical reference garments, we deliver fully customized counter-samples within 7 business days, including custom dye lab-dips.
Multi-Stage Quality Inspection Framework
Every batch undergoes strict 5-point inspection: raw material lab verification, cutting piece audit, inline sewing inspection every 3rd operation, branding alignment audit, and pre-shipment AQL 2.5 final box audit.
Full International Export Compliance
Fully compliant with global trade terms including FOB, CIF, DDP, and DAP. Our experienced export documentation desk handles customs clearance, COO certification, DGFT compliance, and international freight logistics to over 15 countries.
Partner with China's Premier OEM Apparel Manufacturer
Need custom uniform production, private label apparel manufacturing, or technical workwear prototyping? Speak directly with our engineering team today to review tech packs, request fabric swatches, or obtain immediate FOB pricing.
6. Frequently Asked Questions (FAQ) for B2B Apparel Procurement
In-depth answers addressing critical commercial, technical, and operational questions commonly raised by global apparel buyers.
Our standard Minimum Order Quantity (MOQ) is 500 pieces per design/color for custom corporate uniforms and hospitality workwear. For specialized fashion items or private label lines using stock fabric colors, we offer flexible low-MOQ starting points of 200 pieces per style to support brand testing and preliminary market rollouts.
We provide comprehensive branding solutions including high-density embroidery, screen printing (plastisol, water-based, discharge), silicone transfer, heat sublimation, and woven custom neck labeling. Color matching is executed using international Pantone (TCX/TPX) color codes with lab-dip swatches submitted for client sign-off prior to bulk dyeing.
Pre-production sampling typically takes 7 business days following tech-pack and lab-dip approval. Mass bulk manufacturing requires approximately 15 to 25 calendar days, depending on overall order volume, fabric customization complexity, and current facility capacity scheduling.
We operate under the ISO 9001:2015 Quality Management System using strict AQL 2.5 (Acceptable Quality Limit) standards for major defects and AQL 4.0 for minor defects. Every shipment includes an official factory inspection certificate detailing dimensional consistency, stitch density, seam strength, and finishing accuracy.
Yes, absolutely. Our CAD engineering department seamlessly converts client-supplied PDF tech packs, vector files, or physical garment samples into master production patterns. If required, our design team can also assist in drafting technical specs and size charts based on your target market demography.
We routinely execute shipments under FOB (Free on Board), CIF (Cost, Insurance, and Freight), DDP (Delivered Duty Paid), and DAP (Delivered at Place) terms. Our export logistics desk handles all DGFT/IEC documentation, Certificate of Origin (COO), commercial invoices, packing lists, and bill of lading filings for smooth customs entry.
Hospitality and workwear fabrics undergo rigorous pre-shrinkage testing, tensile strength evaluation, anti-pilling treatments (Martindale abrasion test), and washing colorfastness tests (ISO 105-C06 standard). This guarantees garments retain color vibrancy and shape structure after hundreds of industrial wash cycles.
We offer a dedicated line of eco-conscious textiles, including GOTS-certified organic cotton, Recycled Polyester (rPET) derived from post-consumer plastics, naturally anti-bacterial bamboo fiber, and OEKO-TEX Standard 100 certified low-impact dyed fabrics.
Optimize Your Apparel Supply Chain with China's Leading OEM Partner
Get instant factory quotes, request physical fabric swatch books, or schedule a technical consultation with our senior product engineering team. Experiencing unmatched manufacturing precision and reliable delivery key to your brand's growth.