Featured Industrial & Medical Lab Coat Series
Explore our top-tier export lab apparel built for clinical precision, pharmaceutical cleanrooms, modern healthcare facilities, and industrial laboratories.
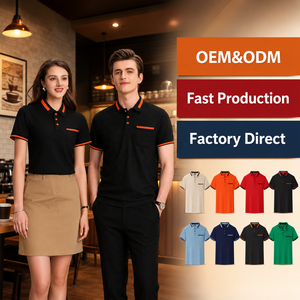
Wholesale Premium Custom Medical Lab Coat Custom Printed & Embroidered Logo
Contact Us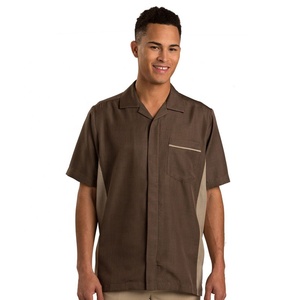
Short Sleeve Medical Staff & Laboratory Technician Scrub Shirt Uniform
Contact Us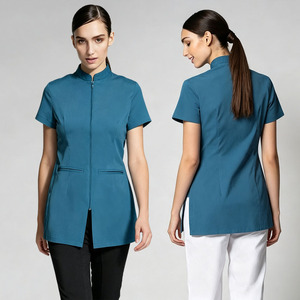
Custom Professional Work Wear Luxury Laboratory & Clinical Spa Uniform for Women
Contact Us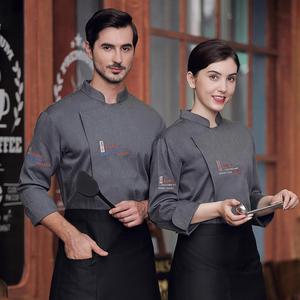
Long Sleeve Chemical Resistant Heavy Duty Laboratory Jacket for Research Institutes
Contact Us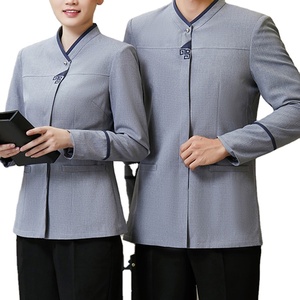
Unisex Professional Laboratory Work Jacket Long Sleeve Protective Lab Coat
Contact Us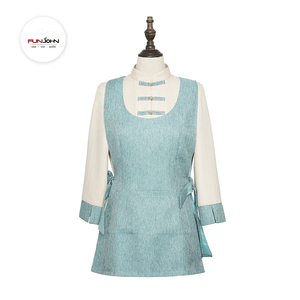
OEM Customized High-Density Polyester Laboratory & Cleanroom Protective Suit
Contact Us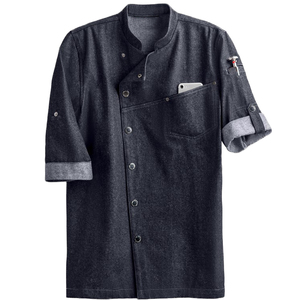
ESD Anti-Static Conductive Fiber Cleanroom Lab Coat Jacket for Semiconductor Plant
Contact Us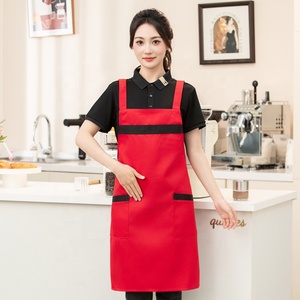
Factory Direct Professional Waterproof & Chemical Splatter Protective Lab Gown
Contact UsWhy Global Healthcare & Scientific Brands Choose Our China Manufacturing Base
As a premier B2B custom lab coat manufacturer, we integrate vertical textile sourcing, CAD-assisted pattern engineering, and international compliance to deliver unrivaled garment performance.
Vertically Integrated Infrastructure
Operating state-of-the-art automated cutting lines, JUKI high-density lockstitch machinery, and computerized embroidery centers, our facility produces up to 50,000 lab coats monthly with absolute dimensional accuracy across sizes XS to 5XL.
Rigorous 5-Stage QC System
Our quality assurance framework spans raw material GSM/colorfastness verification, automated pattern CAD alignment, in-line seam tensile testing, branding precision inspection, and final AQL 2.5 standard audit before export boxing.
Global Trade Compliance
Equipped with complete export licensing, IEC registration, and customs documentation expertise, we guarantee seamless FOB, CIF, and DDP shipments to the USA, UK, EU, Middle East, and Southeast Asia with zero supply chain friction.
End-to-End Precision Quality Engineering
Every bulk order of custom lab coats follows a standardized, fully traceable manufacturing cycle designed for zero-defect compliance.
Fabric Testing
Spectrophotometer color matching, shrinkage resistance evaluation, fluid barrier testing, and GSM verification.
CAD & Cutting
Laser-guided computerized cutting ensuring strict compliance with multi-size ergonomic measurement sheets.
Precision Assembly
Double-needle lockstitching, bar-tacked stress points (pockets/side slits), and anti-puckering collar construction.
Branding QC
High-density Tajima embroidery placement check, Pantone color alignment, and heat-seal durability verification.
AQL 2.5 Audit
Final steam pressing, loose thread trimming, individual polybagging, and master carton drop-test inspection.
Future Procurement Trends in Bulk Custom Lab Coats (2025–2030)
Insights for corporate procurement directors, hospital supply chain executives, and laboratory buyers navigating market shifts.
1. Transition to Smart Functional Fabrics
Global enterprise procurement is rapidly shifting away from conventional 100% cotton uniforms toward advanced composite textiles. Modern institutional buyers require silver-ion antimicrobial treatments capable of enduring 50+ commercial wash cycles, liquid-repellent fluorocarbon-free coatings (AAMI Level 2/3 protection), and integrated conductive carbon threads for electrostatic discharge (ESD) safety in microchip cleanrooms.
2. ESG Mandates & Recycled Polyester Blends
Environmental, Social, and Governance (ESG) compliance has become a mandatory criterion for Tier-1 healthcare systems and European pharmaceutical conglomerates. Manufacturers in China are responding by introducing rPET (Recycled Polyethylene Terephthalate) blended with organic long-staple cotton, certified under GRS (Global Recycled Standard) and OEKO-TEX Standard 100, reducing carbon footprints without compromising fabric durability.
3. Modern Ergonomics & Unisex 3D Tailoring
Traditional stiff, boxy lab coats are obsolete. Future procurement contracts prioritize 4-way stretch mechanical fabrics (Spandex-infused cotton/poly blends), back vent pleats for unrestricted movement during benchwork, hidden magnetic closures replacing breakable plastic buttons, and tailored female silhouettes alongside versatile unisex cuts.
B2B Material Engineering & Fabric Specification Guide
Selecting the appropriate fabric composition, weave density, and finishing treatment based on specific laboratory environments.
| Fabric Composition | Weight (GSM) | Key Technical Properties | Recommended Application | Durability Score |
|---|---|---|---|---|
| 65% Polyester / 35% Cotton Twill | 190 - 240 GSM | High tensile strength, crease resistant, fast drying, industrial wash compatible | Hospital clinical staff, university research laboratories, general medical work | 9.5 / 10 |
| 100% Long-Staple Combed Cotton | 200 - 260 GSM | Maximum breathability, anti-static, heat resistant (flame safe near Bunsen burners) | Chemical synthesis labs, thermal research facilities, high-comfort environments | 8.5 / 10 |
| 99% Polyester / 1% Conductive Carbon Grid | 150 - 180 GSM | Surface resistance 10^6–10^8 ohms, lint-free particle barrier, EN 1149 certified | Semiconductor cleanrooms, microelectronics assembly, pharmaceutical compounding | 9.8 / 10 |
| 72% Poly / 21% Rayon / 7% Spandex | 180 - 220 GSM | 4-way stretch, ultra-soft luxury handfeel, moisture-wicking, antimicrobial protection | Premium private clinics, aesthetic medicine spas, executive medical directors | 9.0 / 10 |
Macro Trends Driving China's Apparel Manufacturing Competitiveness
How digital manufacturing ecosystems and supply chain cluster integration position China suppliers as preferred global OEM partners.
Automated Pattern Grading & Micro-Customization
With the integration of AI-driven pattern nesting software, China OEM manufacturers can rapidly scale custom branding programs. Whether client orders demand customized embroidery logos, custom pantone dye lots, specialized pocket configurations (iPad/tablet sized pockets, pen slots), or contrast piping, automated cutting systems allow low MOQ sampling and seamless high-volume production transitions.
Enhanced Fluid Barrier & Chemical Protection Standards
Post-pandemic safety standards have permanently elevated fluid protection requirements for medical workwear. Modern lab coats incorporate liquid-repellent DWR (Durable Water Repellent) nanotechnology that causes blood, chemical reagents, and aqueous splatters to bead up and roll off the fabric surface, protecting personnel while maintaining air permeability.
Supply Chain Consolidation & Rapid Turnaround
China's centralized textile ecosystems in Guangdong, Zhejiang, and Jiangsu allow seamless integration between yarn spinners, fabric weavers, dye houses, and garment factories. This proximity reduces bulk lead times to 15 to 25 business days, enabling international B2B buyers to maintain lean inventory levels while benefiting from competitive factory-direct wholesale pricing.
Frequently Asked Questions for Bulk Lab Coat Orders
Detailed technical answers to assist procurement managers in evaluating manufacturing capabilities, order procedures, and product specifications.
What is your standard Minimum Order Quantity (MOQ) for custom lab coats?
Our baseline MOQ for standard customized lab coats with custom embroidery/printing is 300 to 500 pieces per design/color, accommodating multiple blended sizes (XS to 5XL). For specialized custom dyed fabric colors or custom woven technical fabrics (such as high-level ESD anti-static cloth), the MOQ is typically 1,000 pieces per order.
Can you provide custom logo application and private label packaging?
Yes. We provide complete OEM/ODM private label solutions including high-density logo embroidery, screen printing, heat transfer labeling, custom woven neck labels, care tags, custom polybags with barcodes, and branded master cartons ready for direct warehouse distribution.
What testing certifications do your laboratory garments meet?
Our fabrics can be engineered to pass international standards including ISO 9001:2015 for quality management, OEKO-TEX Standard 100 for harmful substance safety, EN 1149 for electrostatic properties, and ANSI/AAMI PB70 for liquid barrier performance in healthcare environments.
What is the sample development lead time and mass production timeline?
Pre-production counter samples are developed and dispatched within 5 to 7 business days via express courier (DHL/FedEx). Once sample approval and deposit are confirmed, mass production lead times range between 15 to 25 calendar days depending on total order volume and customization complexity.
How do you guarantee color matching and dimensional stability after industrial washing?
We perform pre-shrunk fabric treatments (sanforization) and utilize reactive dyes with high colorfastness ratings (Grade 4+ against washing and light). All fabric lots undergo laboratory wash testing at 60°C to verify dimensional shrinkage remains strictly below ±3% before cutting begins.
What international shipping terms and payment terms do you support?
We support standard Incoterms including EXW, FOB (Shanghai/Ningbo/Shenzhen), CIF, CFR, and DDP (Delivered Duty Paid directly to your door/warehouse). Accepted payment methods include T/T (Telegraphic Transfer), L/C at sight for large enterprise contracts, and secure trade financing options.
Partner with China's Leading Custom Lab Coat Manufacturer
Get factory-direct B2B pricing, free fabric swatches, and technical consultation for your corporate uniform program today.
Contact Us