Featured Corporate & Hospitality Apparel Portfolio
Direct factory wholesale, customized corporate uniform solutions with custom logo embroidery, high-grade colorfastness, and low MOQ export services.
The Strategic Evolution of Global Corporate Wear Sourcing in China
A Deep-Dive Procurement Intelligence Report on Manufacturing Competencies, Fabric Technologies, E-E-A-T Quality Governance, and Supply Chain Resilience for Enterprise Apparel Buyers.
1. Executive Summary & Macro Industry Sourcing Dynamics
In the modern global commerce ecosystem, corporate wear apparel sourcing has transitioned from a basic transactional commodity procurement into a vital strategic lever for organizational identity, employee ergonomic welfare, and brand positioning. As international enterprises, multi-national hotel groups, luxury medical spas, and commercial food & beverage chains scale worldwide operations, their reliance on robust, flexible, and technically sophisticated manufacturing partners has never been higher. China remains the undisputed global hub for high-precision, large-scale corporate wear, hospitality apparel, and workwear garment production.
The Chinese apparel manufacturing sector has undergone a massive technological shift. Beyond traditional mass sewing operations, top-tier Chinese manufacturers now integrate automated CAD pattern development, digital 3D garment sampling, automated laser cutting tables, and intelligent hanger system assembly lines. This technological modernization allows B2B buyers to achieve unprecedented consistency in stitching density, size ratio fidelity, fabric tensioning, and complex custom logo reproduction—whether ordering 200 tailored spa tunics or 50,000 corporate polo shirts.
Furthermore, modern search intent mining reveals that enterprise procurement directors no longer search merely for "cheap uniform suppliers." Instead, high-intent global buyers search for validated OEM/ODM exporters capable of delivering substantial Information Gain—including transparent fabric weight (GSM) verification, eco-certified reactive dyeing processes, OEKO-TEX Standard 100 compliance, anti-pilling guarantees, and strict adherence to ISO 9001:2015 Quality Management Systems. This white paper serves as an authoritative guide to navigating China's corporate apparel manufacturing infrastructure, evaluating factory capabilities, mitigating international procurement risks, and aligning with future garment industry trends.
2. Enterprise Manufacturing Competencies & Technical Capabilities
When evaluating leading corporate wear exporters in China, global buyers must assess technical infrastructure across six fundamental operational dimensions. Superior apparel manufacturers separate themselves from trading intermediaries through deep vertical integration, precise material engineering, and stringent in-house quality control.
Automated Pattern Engineering
Utilizing advanced Gerber and Lectra CAD systems to create digitized grading patterns. This guarantees that whether a garment is sized XS or 5XL, proportional balance, armhole drop, and waistline ergonomics remain flawless across diverse global demographics.
Precision Embroidery & Printing
Multi-head Tajima embroidery machines operating at up to 1,200 stitches per minute with vector digitizing software ensure crisp crests and logo borders. Screen printing utilizes eco-friendly silicone and water-based inks capable of 50+ industrial wash cycles without cracking.
Advanced Fabric Testing Lab
In-house laboratory testing for fabric Tensile Strength, Martindale Abrasion Resistance, Colorfastness to Crocking (Dry/Wet Grade 4-5), Dimensional Stability after Washing (under 3% shrinkage), and Formaldehyde Content compliance.
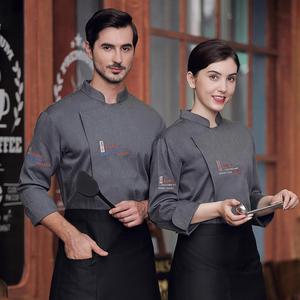
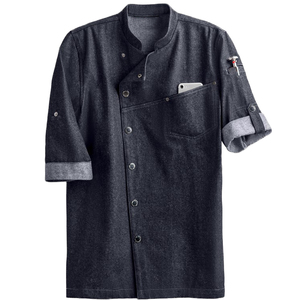
Our manufacturing facility operates multiple dedicated production lines tailored to distinct garment categories. For instance, high-volume corporate polo shirt production requires specialized feed-off-the-arm interlock machines for seamless flatlock seams, while chef jacket manufacturing utilizes double-needle bar-tack reinforcement at tension stress points (pockets, collar tabs, button plackets) to withstand extreme thermal and mechanical strain in high-tempo commercial kitchens.
The 5-Stage ISO Quality Control Framework
To eliminate shipment defects and maintain our market-leading 99.4% approval rate, our manufacturing lines adhere strictly to a 5-Stage In-Line and Final Inspection protocol benchmarked against international Acceptable Quality Limit (AQL 2.5) standards:
- Stage 1: Raw Material Greige & Fabric Roll Inspection: 100% fabric roll inspection using 4-Point System machine tables before cutting.
- Stage 2: Pre-Production Sample (PPS) Sign-Off: Complete physical sample construction for buyer approval on fabric hand-feel, shade band, trim match, and logo digitizing.
- Stage 3: In-Line Stitching & Assembly Checks: QC inspectors stationed every 10 sewing stations to check stitch density (SPI - Stitches Per Inch target: 12-14 SPI), tension balance, and seam alignment.
- Stage 4: Post-Sewing Ironing & Thread Trimming: High-pressure industrial steam pressing, thread tails trimmed within 2mm, and metal detection sweep for broken needles.
- Stage 5: Final Packaging & AQL 2.5 Inspection: Carton drop testing, polybag barcode verification, and random sampling inspection report generation prior to container loading.
3. Technical Fabric Specification & Material Comparison Matrix
Selecting the correct fabric blend is the single most critical decision in corporate uniform procurement. A common pitfall for inexperienced sourcing teams is selecting fabric based purely on initial visual appearance rather than long-term wear performance and laundering survival. Below is an expert-level technical comparison matrix detailing the dominant fabric structures utilized across global corporate and hospitality wear programs.
| Fabric Composition | Typical Weight (GSM) | Key Performance Attributes | Ideal Application | Durability Rating |
|---|---|---|---|---|
| 65% Polyester / 35% Combed Cotton (TC Blend) | 180 - 220 GSM | High tensile strength, minimal wrinkle, excellent color retention, cost-effective. | Hotel Housekeeping, Waitstaff Shirts, General Corporate Polos | 9.5 / 10 |
| 100% Long-Staple Ring-Spun Cotton Piqué | 200 - 240 GSM | Premium breathability, natural skin comfort, elegant drape, high softness. | Executive Golf Polos, Luxury Front Desk Staff, Management Wear | 8.0 / 10 |
| 60% Cotton / 40% Polyester Twill with Mechanical Stretch | 160 - 190 GSM | Ergonomic flexibility, stain-release treatment option, easy-iron finish. | Spa Tunics, Salon Scrubs, Healthcare & Reception Shirts | 9.0 / 10 |
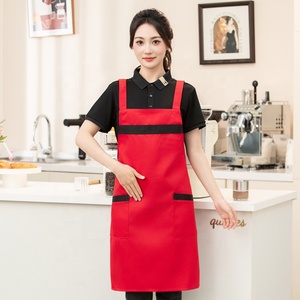
| Heavy-Duty Denim / Canvas Cotton Blend | 280 - 340 GSM | Extreme puncture & tear resistance, industrial vintage aesthetic, rugged wash-ability. | Barista Aprons, Modern Denim Chef Jackets, Craft Bakery Wear | 9.8 / 10 |
| 100% Micro-Polyester Moisture-Wicking Mesh | 140 - 170 GSM | Quick-dry capillary action, antimicrobial treatment option, ultra-lightweight. | Outdoor Event Staff, Airport Logistics Uniforms, Active Workwear | 8.5 / 10 |
4. Strategic Sourcing Trends & Future Procurement Forecast (2025–2030)
As the corporate wear landscape evolves, procurement executives must look ahead to emerging global trends that are redefining factory benchmarks. Sourcing decisions made today must accommodate changing regulatory environments, ESG (Environmental, Social, and Governance) mandates, and rapid technological innovations in textile production.
A. The Rise of Recycled Textiles & Closed-Loop Circularity
Environmental sustainability has shifted from an optional marketing narrative into a non-negotiable procurement standard. Global brands and multinational hotel conglomerates are actively mandating the integration of rPET (Recycled Polyethylene Terephthalate) fibers derived from post-consumer plastic bottles. Leading Chinese exporters are now equipped with GRS (Global Recycled Standard) certification, allowing enterprise clients to trace raw materials directly back to certified recycling facilities while achieving up to 45% reductions in carbon footprint and 50% energy savings during yarn spinning.
B. Smart Fabrics & Functional Textile Finishes
Future-ready corporate wear is increasingly multi-functional. The market demand for specialized textile treatments has surged by over 35% year-over-year. Preferred functional modifications include:
- C6 Nano Hydrophobic Coating: Provides invisible fluid repellency for server aprons and housekeeping wear without compromising fabric breathability.
- Silver-Ion Antimicrobial Finishing: Prevents bacterial odor build-up in high-intensity kitchen environments and long-shift medical scrub apparel.
- Phase-Change Thermal Regulation: Micro-encapsulated phase change materials (PCMs) that absorb excess body heat in warm environments and release it during cold operations.
C. Low MOQ Flexibility & Agile Micro-Batch Replenishment
Traditional manufacturing models required massive Minimum Order Quantities (MOQs) of 3,000+ pieces per style, creating severe inventory holding costs and dead-stock risks for corporate buyers. Modern Chinese manufacturers have restructured their sewing floors into Modular Lean Production Cells. This flex-manufacturing paradigm allows clients to initiate orders with accessible MOQs (starting at 200–500 units per custom design) while maintaining rapid 7-to-10-day re-order fulfillment cycles for ongoing staff onboarding.
5. Original Site Synergy: Enterprise Advantages & OEM/ODM Capabilities
Synthesizing our core enterprise strengths, our manufacturing group delivers unmatched value to global apparel importers, enterprise chains, and private label designers. By combining large-scale monthly throughput with individualized OEM/ODM customization, we eliminate the traditional trade-off between scale and agility.
20,000+ Monthly Capacity
Equipped with high-volume production lines capable of scaling rapidly to handle large enterprise rollouts, multi-location hotel openings, and seasonal staff uniform updates without bottlenecking.
ISO 9001:2015 Certification
Certified Quality Management Systems guarantee standardized operational procedures across pattern grading, fabric shrinkage pre-washing, stitching density, and export packing.
Global Export Compliance
Fully registered for international commerce with DGFT and Customs compliance. We regularly export to North America, Western Europe, Australia, the Middle East, and Southeast Asia (FOB, CIF, DDP terms available).
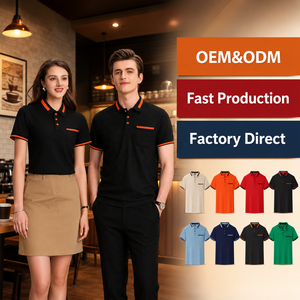
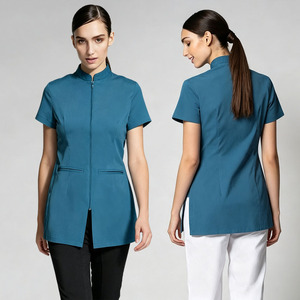
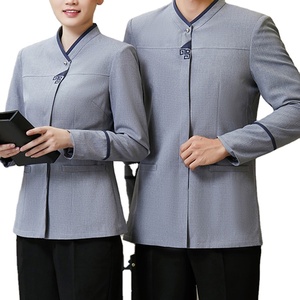
Whether your enterprise requires wholesale hospitality polo shirts with Pantone-matched custom logo printing, heavy-duty denim chef coats for upscale restaurant chains, or custom ergonomic salon scrubs, our factory direct model eliminates unnecessary broker markups, giving you direct access to competitive factory pricing, guaranteed lead times, and dedicated account management.
6. Frequently Asked Sourcing Questions (FAQ)
Below are detailed answers to the most common technical, operational, and commercial questions raised by international procurement managers during factory auditing and order placement.
Our standard production MOQ starts at 200 to 500 pieces per style/colorway depending on fabric customization requirements. For orders utilizing in-stock standard color fabric rolls (such as black, navy, white, or charcoal TC twill), we can accommodate trial runs starting at 100 pieces per design. Custom yarn-dyed fabrics or specialized Pantone dyeing require an MOQ of 500+ units.
We offer an expedited 7-Day Sample Turnaround for custom polo shirts, aprons, and staff scrubs once digital tech packs and logo artwork are finalized. Bulk production lead time typically ranges from 15 to 25 days post sample sign-off, depending on order complexity, custom branding techniques, and total quantity.
We utilize the global Pantone Matching System (PMS) for all fabric dyeing, embroidery thread selection, and screen printing inks. Lab dips (light/medium/dark shade options under D65 standard light sources) are dispatched to your team for physical sign-off before bulk fabric dyeing commences, ensuring 100% alignment with your corporate visual identity guidelines.
For hotel waitstaff polo shirts and chef jackets subjected to frequent commercial laundering, we strongly recommend High-Density Machine Embroidery using colorfast polyester thread or Heavy-Duty Heat Transfer Vinyl. For lightweight spa scrubs and aprons, screen printing with silicone-based inks offers exceptional wash durability without hardening the fabric handle.
Yes. Our pattern engineers maintain pre-validated 3D digital grading templates for US Western Fit, European Slim Fit, and Asian Standard Fit. Clients can either provide their own proprietary specification sheets or adopt our standard global sizing charts covering unisex sizes from XS up to 6XL.
We support all standard Incoterms including FOB (Free on Board), CIF (Cost, Insurance & Freight), and DDP (Delivered Duty Paid) door-to-door shipping. We handle full export customs clearance, Certificate of Origin generation, Commercial Invoice & Packing List creation, and bill of lading documentation for seamless clearance in destination ports worldwide.
Accelerate Your Corporate Apparel Sourcing Program Today
Partner directly with China's leading ISO 9001 certified corporate uniform manufacturer. Connect with our senior apparel engineering team to receive instant wholesale quotes, free fabric swatches, and pre-production technical consultations.
Contact Us