1. Executive Sourcing Guide: CE Certified Luxury Hotel Robes & Hospitality Apparel Architecture
In the global luxury hospitality landscape, procurement managers and supply chain directors face a dual challenge: elevating guest touchpoint luxury while guaranteeing rigorous cost per wash cycle efficiency. As an established export manufacturer operating from Gurgaon, Delhi NCR, India, Vihaan International engineers high-performance luxury hotel bathrobes and hospitality staff uniforms tailored to five-star resorts, wellness spas, boutique retreats, and international hotel groups across North America, Europe, and the Middle East.
The benchmark for commercial bathrobes has evolved beyond simple softness. Today's procurement specifications require strict adherence to CE Certification frameworks (EN ISO 13688 standards for general protective clothing and EN 14878 flammability standards), ensuring chemical safety, textile skin compatibility, zero hazardous azo dyes, and fire-safety compliance for guest safety. When sourcing CE certified luxury hotel robes bulk factories & exporter partners, procurement officers must evaluate not only stitch density and fabric weight (GSM), but also structural tensile resilience against commercial tunnel washers and high-temperature rotary dryers.
1.1 Fabric Weave Mechanics: Zero-Twist Combed Cotton vs. Waffle Weave vs. Micro-Velour
Selecting the appropriate weave construction is the foundational decision in bathrobe engineering. Each material profile serves distinct operational environments within a hotel property:
- Zero-Twist Plush Combed Cotton (400 - 550 GSM): Utilizing long-staple Egyptian or Indian cotton fibers, zero-twist yarns permit ambient air to fill the spaces between fibers. This produces an extraordinarily soft, plush hand-feel with instantaneous moisture absorption (<3 seconds per DIN 53924), ideal for presidential suites and VIP guest room amenities.
- Double-Faced Micro-Velour Composite (350 - 420 GSM): Featuring a sheared micro-velour exterior for sleek aesthetic luxury paired with a absorbent terry loop interior. This composite architecture resists chemical degradation from spa massage oils while reducing drying energy expenditure by up to 28% in commercial laundries.
- Diamond & Square Waffle Weave (220 - 300 GSM): Engineered with 100% pre-shrunk combed cotton, waffle robes offer lightweight breathability, rapid drying, and compact storage. Recommended for poolside cabanas, thermal spa circuits, and tropical resort climates.
1.2 Commercial Technical Specification & Performance Benchmark Matrix
| Fabric Type & Weave | GSM Range | Tensile Strength (N) | Water Absorption | Wash Durability Cycle | Recommended Deployment |
|---|---|---|---|---|---|
| Zero-Twist Terry Cotton | 450 - 550 GSM | ≥ 450 N (Warp) / 380 N (Weft) | < 2.5 Seconds | 180 - 220 Industrial Washes | 5-Star Luxury Suites & VIP Rooms |
| Velour / Terry Dual-Layer | 380 - 450 GSM | ≥ 480 N (Warp) / 410 N (Weft) | < 3.0 Seconds | 250+ Industrial Washes | Hotel Spas & Wellness Resorts |
| Pre-Shrunk Cotton Waffle | 240 - 300 GSM | ≥ 400 N (Warp) / 350 N (Weft) | < 4.0 Seconds | 200 - 240 Industrial Washes | Tropical Pools, Saunas & Fitness |
| Microfiber Luxury Shell | 300 - 360 GSM | ≥ 520 N (Warp) / 460 N (Weft) | < 3.5 Seconds | 300+ Industrial Washes | High-Occupancy Executive Properties |
2. Manufacturing Tech & Quality Engineering Standards: The Gurgaon Facility Advantage
Vihaan International's manufacturing facility located in Udyog Vihar Phase 4, Gurgaon, Delhi NCR, is an ISO 9001:2015 certified plant operating integrated production divisions. Spanning state-of-the-art CAD pattern drafting, computerized JUKI and Brother industrial sewing lines, laser edge-cutting, and automated embroidery systems, our factory delivers a consistent monthly output of 20,000+ completed garments and bathrobes.
Double-Needle Seam Reinforcement
All sleeve joins, armholes, pocket perimeters, and belt loop anchors utilize double-needle safety stitching with high-tenacity polyester threads, mitigating seam rupture during high-speed industrial extraction.
Precision Logo Embroidery
Multi-head Tajima embroidery machinery applies brand crests using chlorine-resistant, colorfast threads capable of enduring 90°C thermal disinfection and chemical bleaching processes without fading.
5-Point ISO Quality Protocol
Every batch undergoes incoming fabric inspection, cutting precision check, mid-line sewing audit every 3rd operation, branding alignment audit, and final AQL 2.5 export packaging verification.
Our compliance profile covers full DGFT (Directorate General of Foreign Trade) compliance and IEC (Import Export Code) registration. We provide direct FOB (Freight on Board), CIF (Cost, Insurance, Freight), and DDP (Delivered Duty Paid) door-to-door shipping solutions to buyers in the United States, United Kingdom, European Union (Germany, France, Netherlands), United Arab Emirates, Saudi Arabia, Canada, and Australia.
3. Global Procurement Trends in Hospitality Apparel (2026 – 2030 Roadmap)
Analyzing data from international hotel purchasing associations and global textile trade flows reveals five decisive structural shifts shaping bulk hotel apparel procurement over the coming decade:
Trend 1: Eco-Luxury & GOTS Organic Traceability
Leading hotel chains (Marriott, Hilton, Accor, Hyatt) are setting strict Scope 3 carbon reduction targets. Procurement standard operating procedures now mandate OEKO-TEX Standard 100 Class I certification and GOTS-certified organic cotton fibers, ensuring chemical-free contact with guest skin and audited eco-friendly dyeing processes.
Trend 2: RFID Inventory Micro-Chip Embedding
High-volume resort operations are embedding heat-resistant, washable UHF RFID chips into bathrobe collar seams and staff uniform hems. This enables real-time inventory tracking, reducing loss rates by up to 45% and optimizing commercial laundry billing cycles.
Trend 3: Antimicrobial & Odor-Shield Finishes
Post-pandemic hygiene protocols have popularized non-leaching silver-ion and zinc-pyrithione fabric treatments. These treatments inhibit bacterial proliferation within damp bathrobe terry loops, preserving freshness across multiple guest uses between wash cycles.
Trend 4: Cross-Functional Departmental Uniform Modular Systems
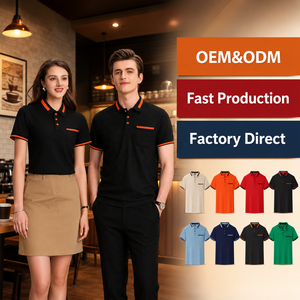
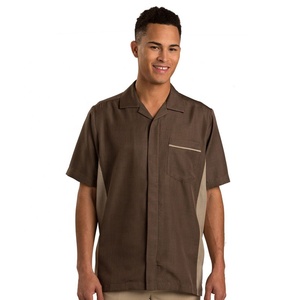
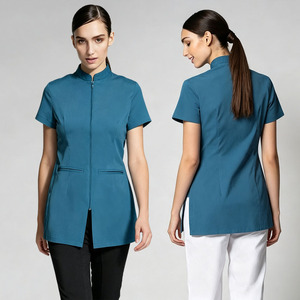
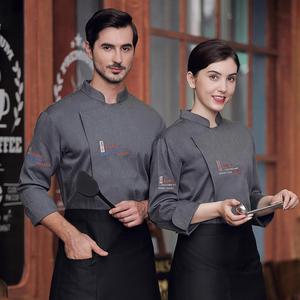
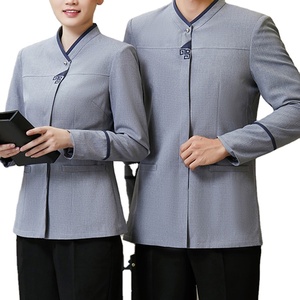
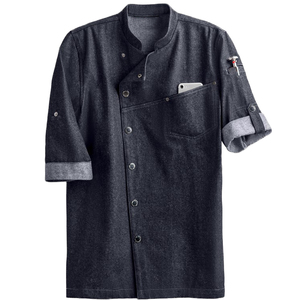
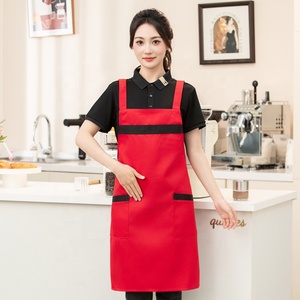
Hospitality operators are abandoning fragmented uniform purchasing in favor of cohesive design programs. From front desk polo shirts to kitchen chef coats, housekeeping scrubs, and spa bathrobes, unified color palettes and matching brand trims enhance property brand equity.
4. Bulk Sourcing FAQs: Expert Answers for Hotel Procurement Managers
Our luxury hotel bathrobes and hospitality workwear comply with CE EN ISO 13688 (General Apparel Safety Requirements), EN 14878 (Nightwear and Robe Flammability Standard), and OEKO-TEX Standard 100 Class I (guaranteeing zero harmful heavy metals, pesticides, or formaldehyde). In addition, our manufacturing facility operates under audited ISO 9001:2015 Quality Management Systems.
For standard corporate uniforms and custom hotel robes, our flexible bulk production MOQ starts from 500 pieces per design (200 pieces for specialized private label fashion collections). Pre-production physical samples are delivered within 7 business days following Pantone color lab-dip signoff. Bulk order production lead time ranges between 15 to 25 calendar days depending on embroidery complexity and total volume.
All our cotton terry, velour, and waffle fabrics undergo controlled pre-shrunk sanforization treatment prior to pattern cutting. This mechanical process stabilizes dimensions, restricting total residual shrinkage to under <3% under standard commercial wash procedures (60°C–80°C wash cycles), ensuring collar alignment and sleeve length remain intact over extended usage.
Yes, we offer complete OEM/ODM full-package manufacturing (FPP). This encompasses custom sizing charts (US, EU, Asian, Middle Eastern fits), custom woven brand labels, satin care labels with multi-lingual wash instructions, custom logo polybags, barcode hangtags, and outlet-wise carton packaging for seamless hotel group distribution.
5. Enterprise Sourcing & Manufacturer Partnership Advantage
Selecting Vihaan International as your primary manufacturing partner provides direct factory pricing, eliminating intermediary trading markup while granting complete visibility over raw material sourcing, weaving density, and quality inspection. Founded in 2020 and headquartered in Gurgaon, India, our team combines decades of senior apparel engineering expertise with responsive international trade support.
Whether you are opening a new 5-star hotel property, refreshing room amenities for an established resort chain, or building an international uniform distribution program, Vihaan International delivers uncompromised quality, strict deadline reliability, and full CE/ISO certification compliance.